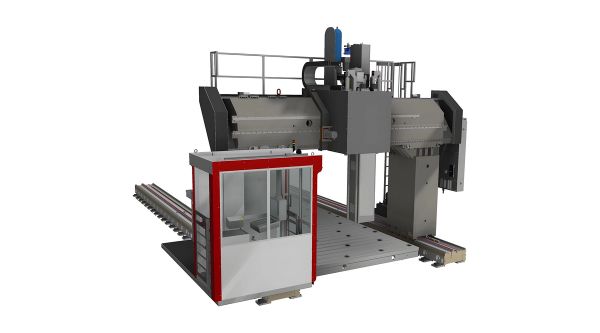
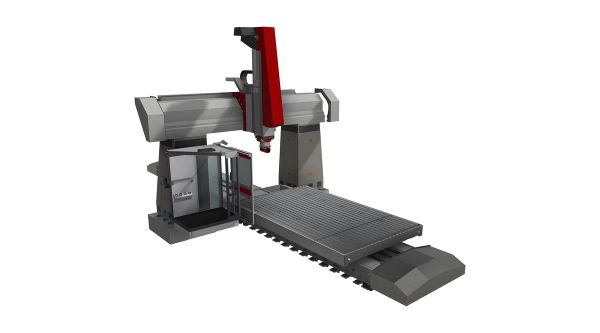
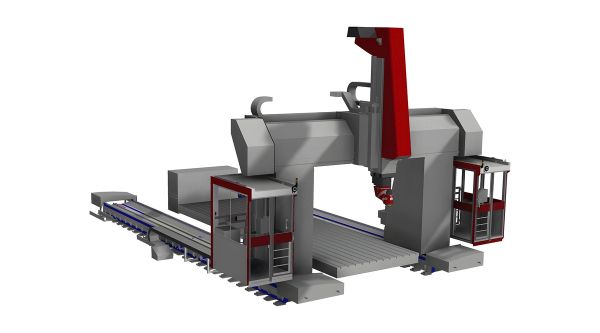
WFT 10/11 (L)
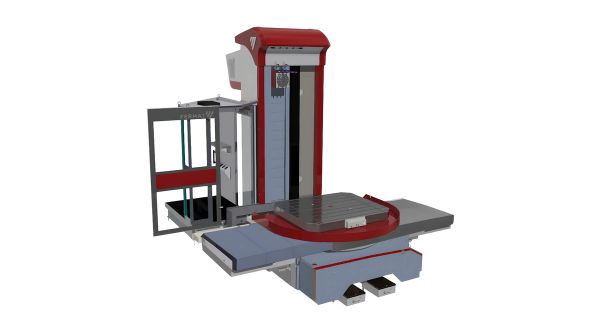
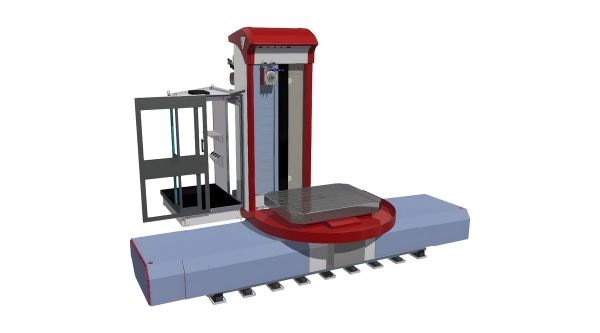
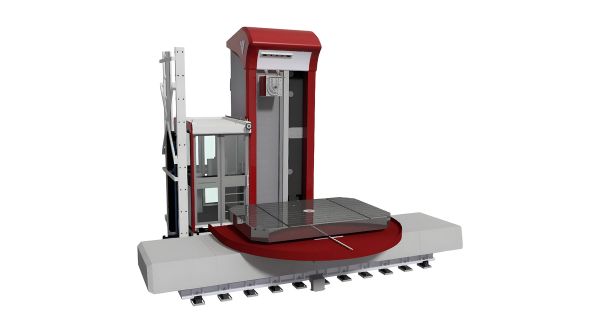
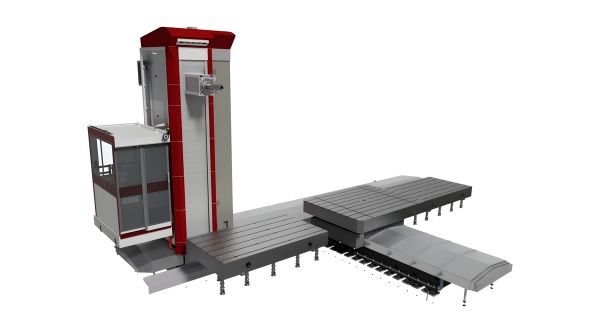
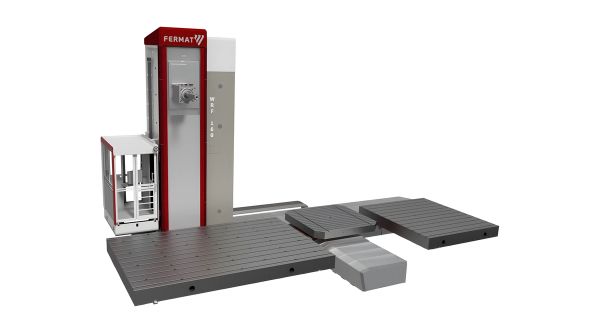
Series · WFT 10/11- Table-type layout, 10 000–20 000 kg table — The T10 table is standard at 10 000 kg; the optional longer X axis (3, 4 or 5 m) takes it to 20 000 kg, and a pallet change system keeps the spindle cutting while the next part is set up.
- Ø 100/110 mm spindle, 730 mm stroke — Two-stage gearbox and three-belt drive up to 4 000 rpm — 5 000 rpm optionally — with a 250 mm support sleeve supplied as standard.
- Active thermal compensation — Spindle dilation in the Z axis is compensated automatically, using four headstock temperature sensors and an air/oil-cooled gearbox to keep bearing temperature stable.
- ATC or robot tool change — ATC for 20/30/40 tools exchanging into spindle or head, or a robot changer with up to 96 tools reaching virtually any head position.
Overview
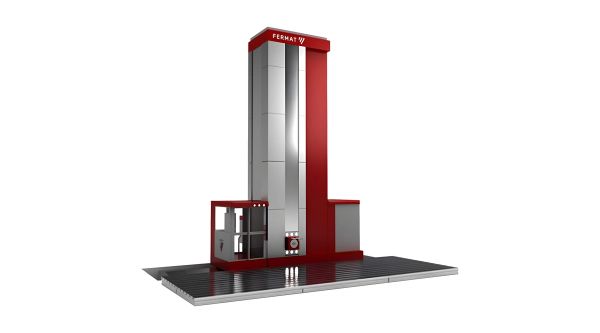
The WFT 11 is a table-type horizontal boring and milling machine for parts too heavy to move once clamped, such as long weldments and complex welded frames. The column travels in Z on its own carriage while the rotary table carries the part across it. Table load is 10 000 kg as standard, or 20 000 kg with the optional longer X axis (3, 4 or 5 m); a pallet change system is available to keep the spindle cutting while the next part is set up. Headstock, column, beds and tables are designed and built by FERMAT in-house, keeping accuracy repeatable and spares on the shelf.
Explore WFT 10/11 (L)
Full technical specifications. Toggle between metric and imperial units.
| Parameter | Units | WFT 10/11 | WFT 10/11 L |
|---|---|---|---|
| Spindle diameter | mm | 100/110 | |
| Spindle taper | — | SK 50 (DIN, MAS 45°, ANSI) | |
| Spindle speed (max.) | rpm | 4000 (opt. 5000) | |
| Main Power Heidenhain or SIEMENS CNC (S1/S6-40%) | kW | 31/46.5 | |
| Max. Torque Heidenhain or SIEMENS CNC (S1/S6-40%) | Nm | 1416/2124 | |
| Main Power FANUC CNC (S1/S3-60%) | kW | 30/37 | |
| Max. Torque FANUC CNC (S1/S3-60%) | Nm | 1370/1692 | |
| X-axis Cross Travel of Table | mm | 2000/3000 (T10); optional 2000/3000/4000/5000/6000 (T20) | |
| Y-axis Vertical Travel of Headstock | mm | 1250/1700/2000 | |
| Z-axis Longitudinal Travel of Column | mm | 1250/1700 | 1500 |
| W-axis Spindle Travel | mm | 730 | |
| Rapid Feed X, Y, Z | mm/min | 12000/12000/8000 | 12000 |
| Rapid Feed W | mm/min | 8000 | 12000 |
| Rapid Feed B | rpm | 2 (opt. 5) | |
| Max. Table Load | kg | 10000 (opt. 20000) | |
| Table Size | mm | 1200×1200 / 1200×1400 / 1400×1600 / 1600×1600 / 1400×1800 / 1600×1800 — optional: 1600×1800 / 1800×2200 / 1800×2600 / 2000×2400 / 2500×2500 / 2000×3000 | |
Customize WFT 10/11 (L)
Pick a category to see compatible accessories. Click any accessory to open its detail window.
Angle Heads & Facing Heads
Manual or automatic angle heads and facing heads for extended machining capability — UHAmi, UHA, PHA, PHAmi, OHA series and more.
Showing 6 of 6
Technology & Software
Smart technologies, control platforms and multitasking capabilities available on this machine. Click any item for details and the full list of compatible machines.
Smart Technologies
Explore smart technologies3D Kinematic Calibration
Measure and correct the machine's kinematic transformation — restores accuracy to the rotary axes without waiting for service.
Vibration Monitoring
Sensors on the spindle and ram watch vibration levels in real time — protecting the machine, the tool and the surface finish.
Adaptive Feed Control
The CNC adjusts feed rate in real time based on spindle load — shorter cycle times in light cuts, tool protection in heavy ones.
Machine Collision Monitoring
The control knows the shape of the machine and stops it before it hits itself — in automatic mode and while jogging by hand.
Spindle Temperature Compensation
Thermal sensors track spindle growth and the CNC compensates automatically — stable accuracy from the first part of the shift to the last.
Multitasking
Explore multitaskingTurning Table
Rotary table rated for turning operations — turn large flanges and rings on the boring mill, no second machine needed.
Interpolation Turning
The spindle interpolates X and Y axes in a circular path to turn features anywhere on the workpiece — without rotating the part.
Facing Head Turning
A facing head with CNC U-axis turns external and internal diameters, faces and tapers — contour turning directly from the spindle.
Software & Control
Compare control systemsEASYCRAFT
FERMAT's own conversational control — guided workshop programming of boring and milling cycles without G-code.
FANUC
Robust FANUC CNC in three tiers — FERMAT FANUC, 30i-B Plus and 31i-B Plus — for maximum reliability and worldwide service.
HEIDENHAIN
Premium HEIDENHAIN Klartext controls — TNC 640, TNC7 and TNC7 Basic — for die & mould and high-precision contouring.
SIEMENS SINUMERIK ONE
The digital-native SINUMERIK ONE — top-end Siemens platform with digital-twin capability.
WFT 10/11 (L) Customer Stories
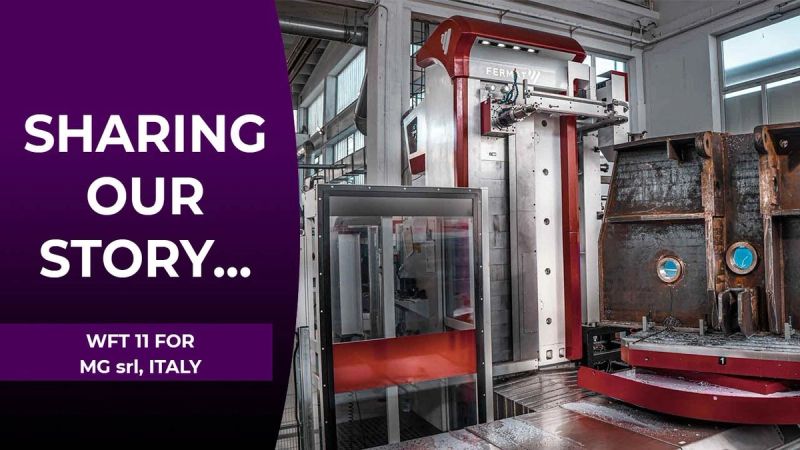
MG srl
MG srl, a leading European maker of plate-roll and section-bending machines, chose a FERMAT WFT 11 to machine frames, bearing supports and bases for its rolling machines in-house.
Read story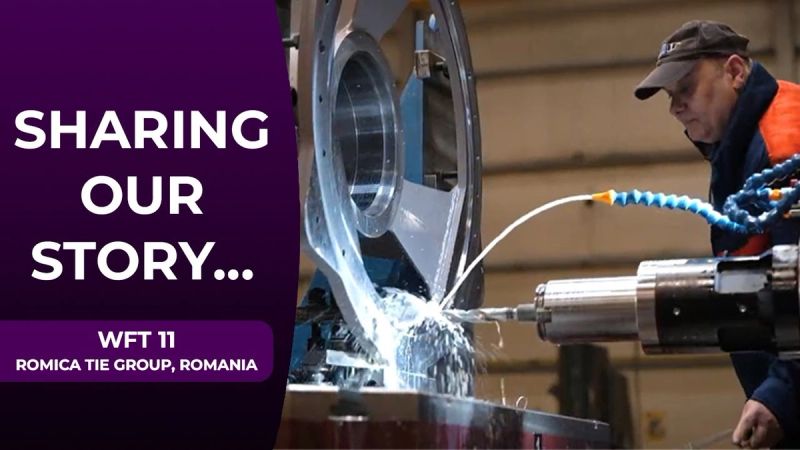
TIE Services International
TIE Services International using FERMAT WFT 10/11 (L) for their energy and power operations in Romania.
Read storyWFT 10/11 (L) FAQ
Procurement and engineering questions we hear about this model.
What is the difference between the WFT 11 and the cross-type WFC?
How big a workpiece can the WFT 11 take?
What spindle is fitted to the WFT 11?
Why is the boring spindle belt-driven rather than direct-driven?
What is the machine structure made of?
How does the machine hold accuracy as it warms up?
How is the rotary table positioned and clamped?
How are automatic milling heads mounted?
Which milling heads fit the WFT 11?
What is the lead time for this machine?
Related Models
Get a tailored proposal for WFT 10/11 (L)
Our engineers spec the exact configuration for your application. We reply within 24 hours.