
 Français
 L'italiano
 Magyar
 Deutsch
 Polski
 Română
 Español
 Українська
 Čeština
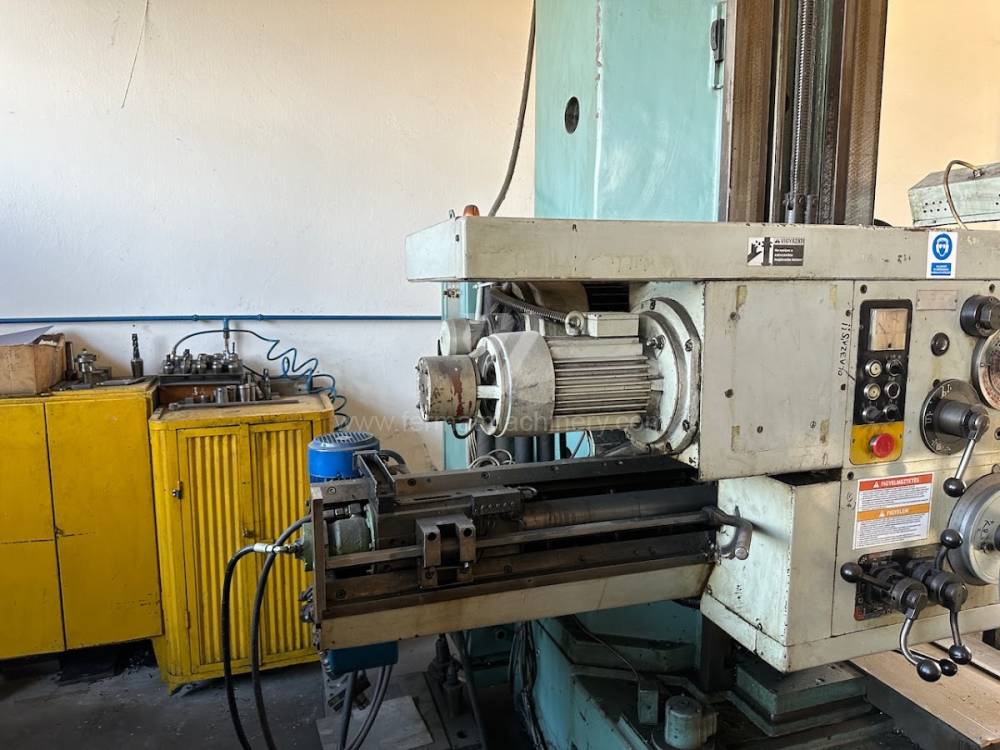
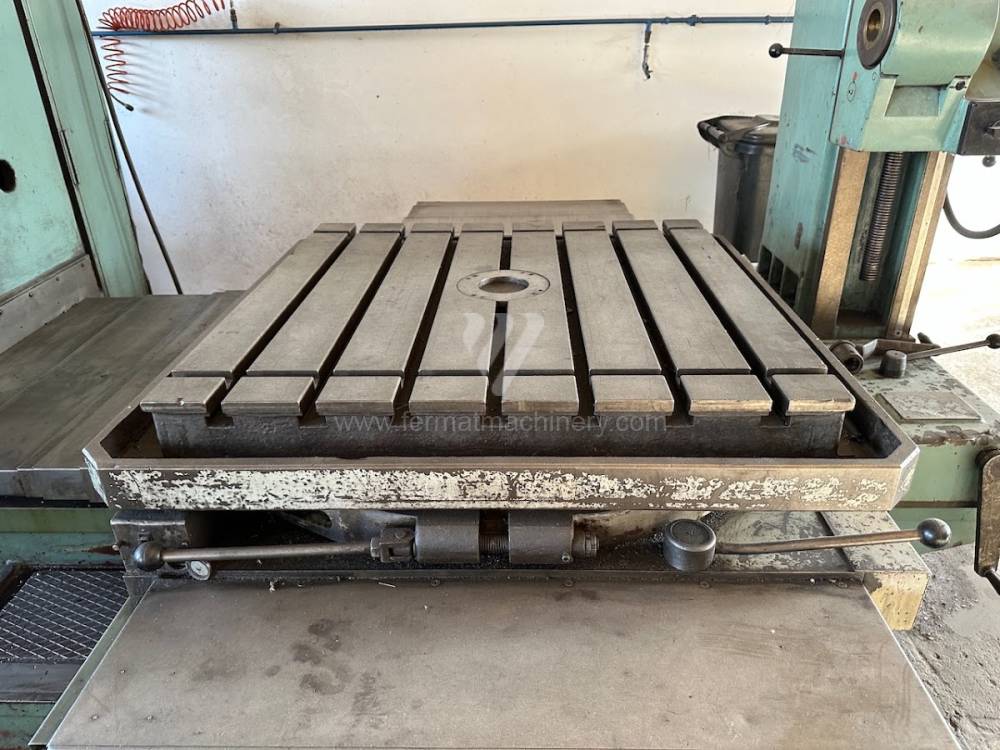
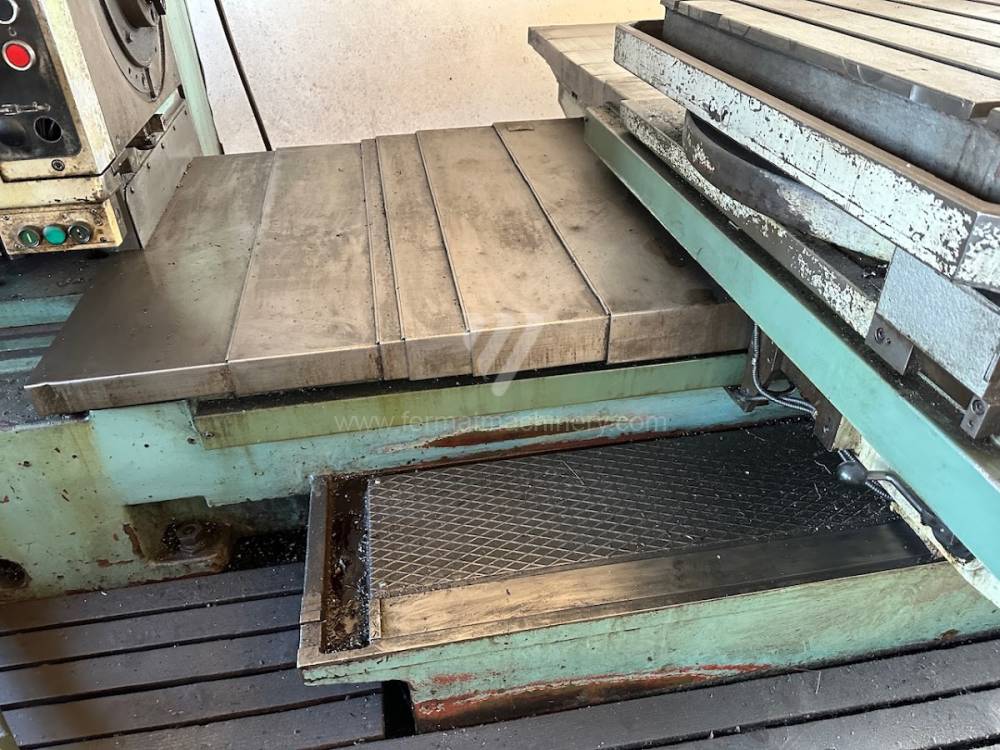
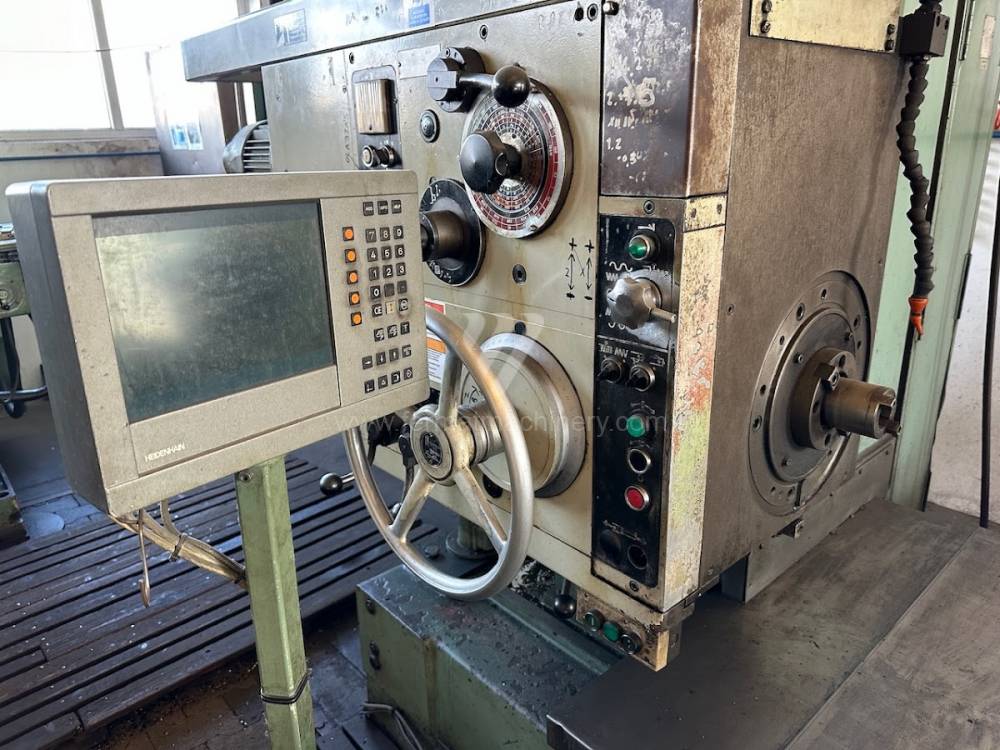
 Borers horizontal
 +420 778 547 838
 info@fermat.cz
Borers horizontal
| Name of a product | Inventory number | Producer | YOM | Parameters | ||
|---|---|---|---|---|---|---|
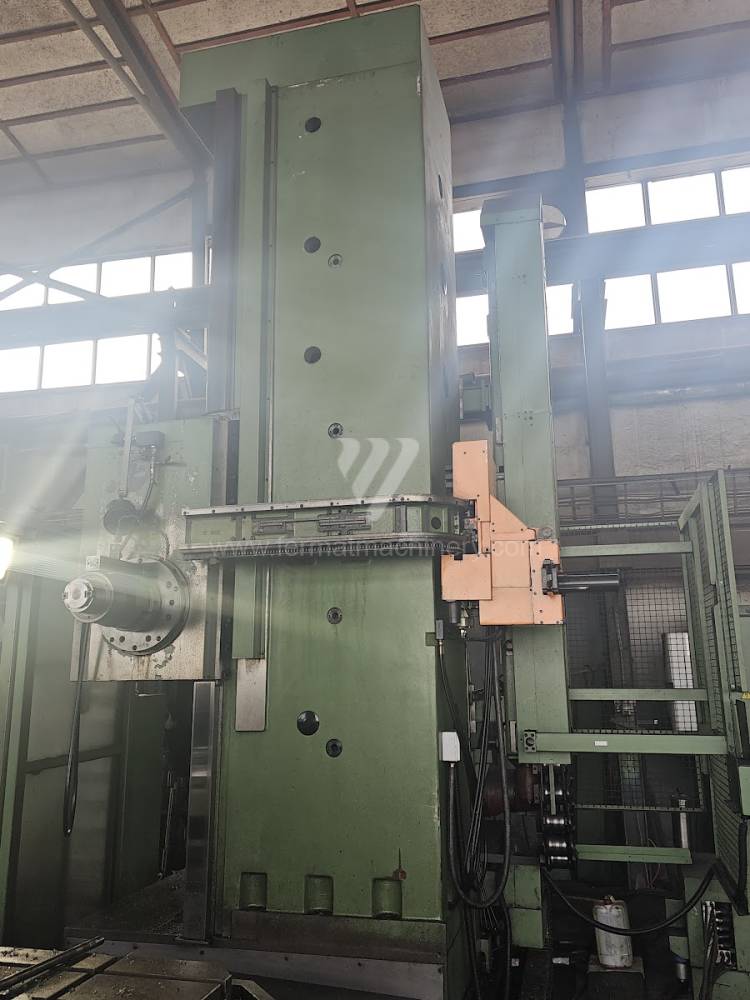 |
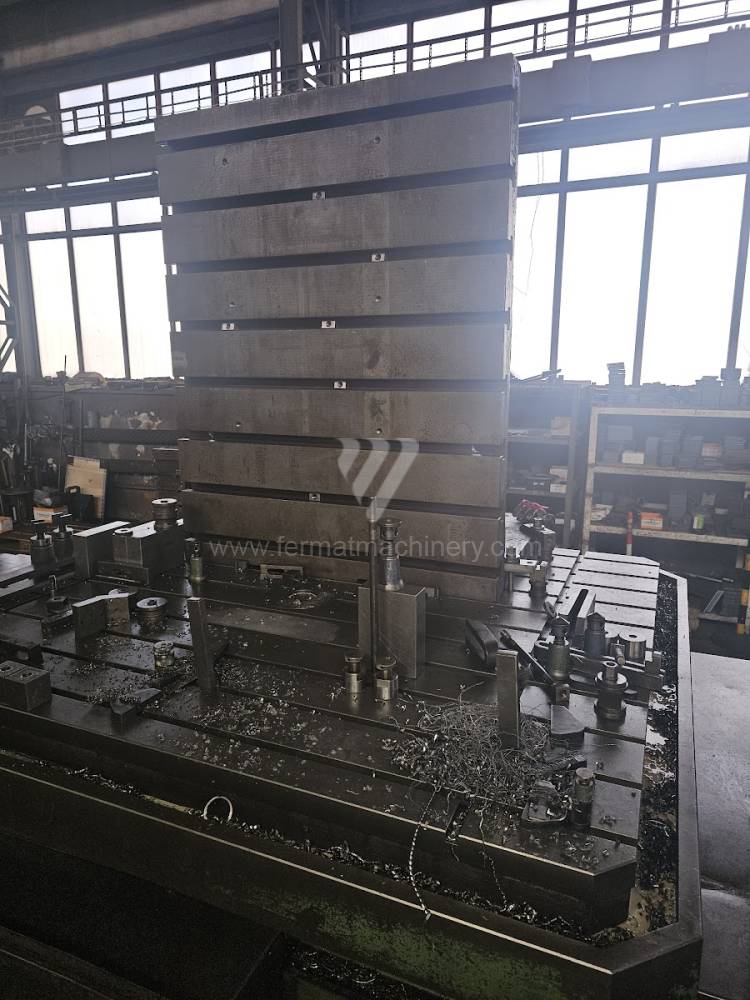
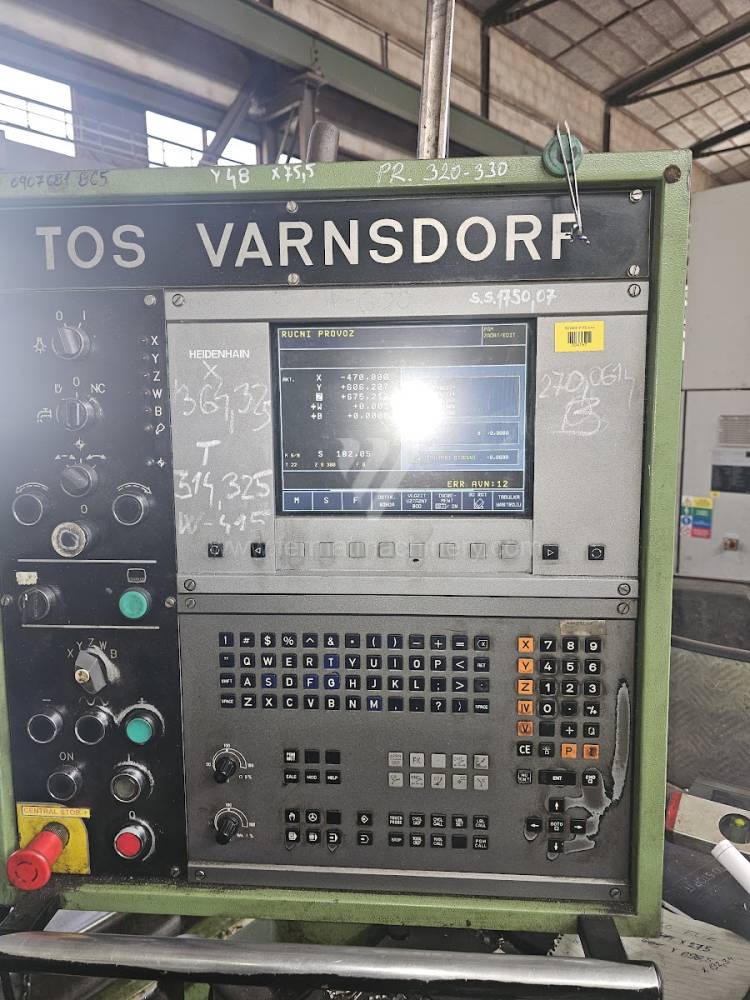
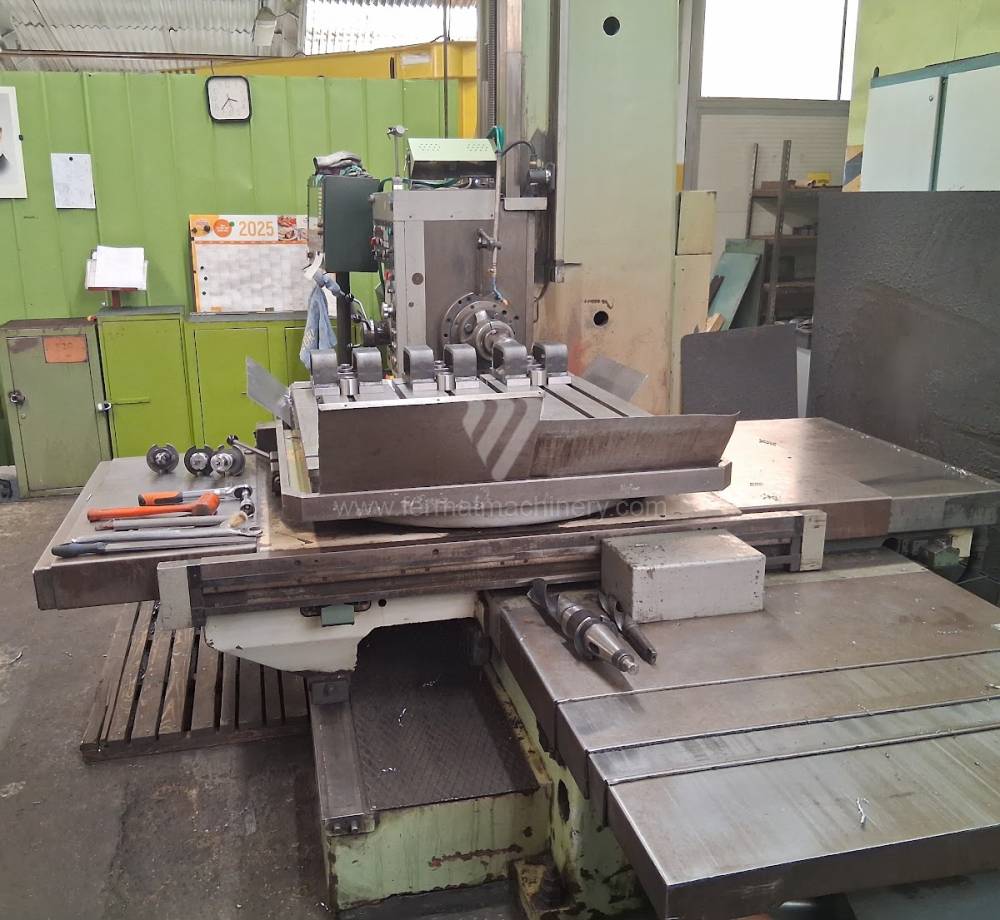
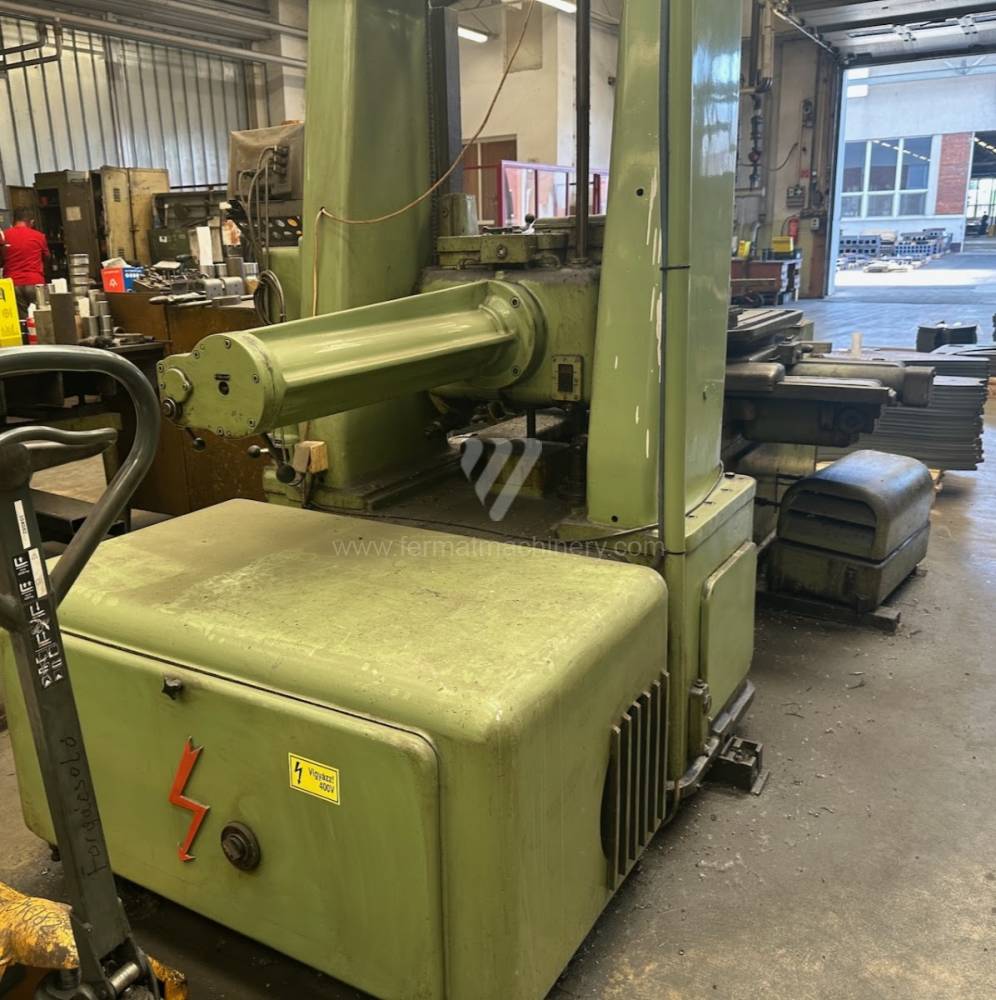
WHQ 13.8 CNC |
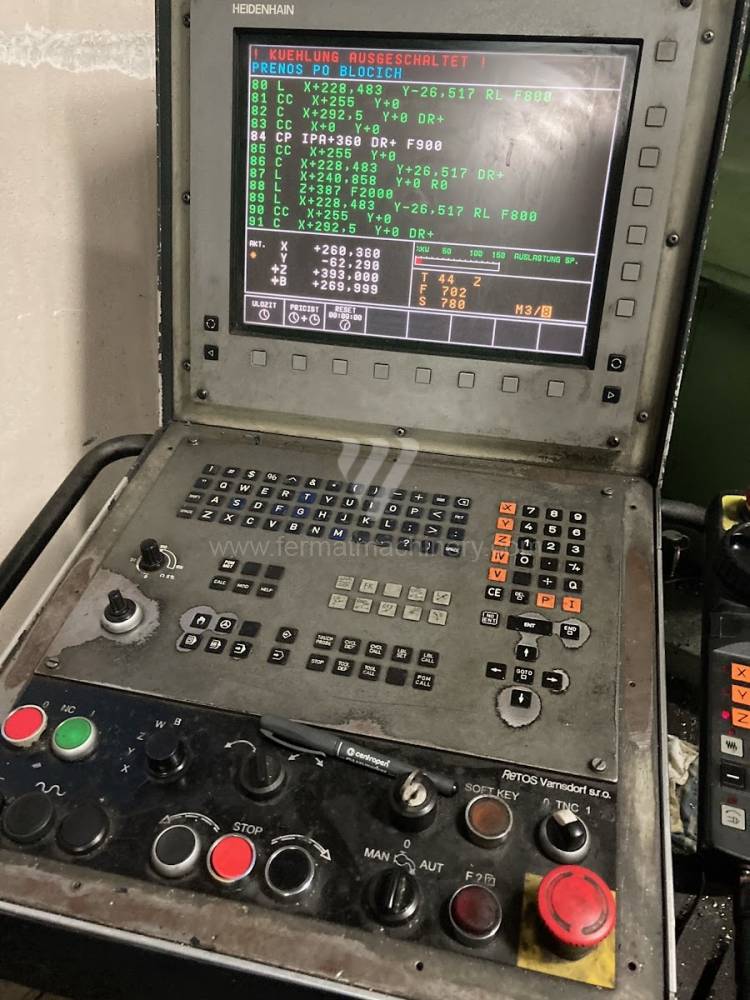
261298 | TOS Varnsdorf | 1999 | Control system Heidenhain: TNC 426 Diameter of working spindle: 130 mm Travel X-axis: 3500 mm Travel Y-axis: 2000 mm Spindle speed: 0 - 1500 /min. Cooling through spindle: NO |
|
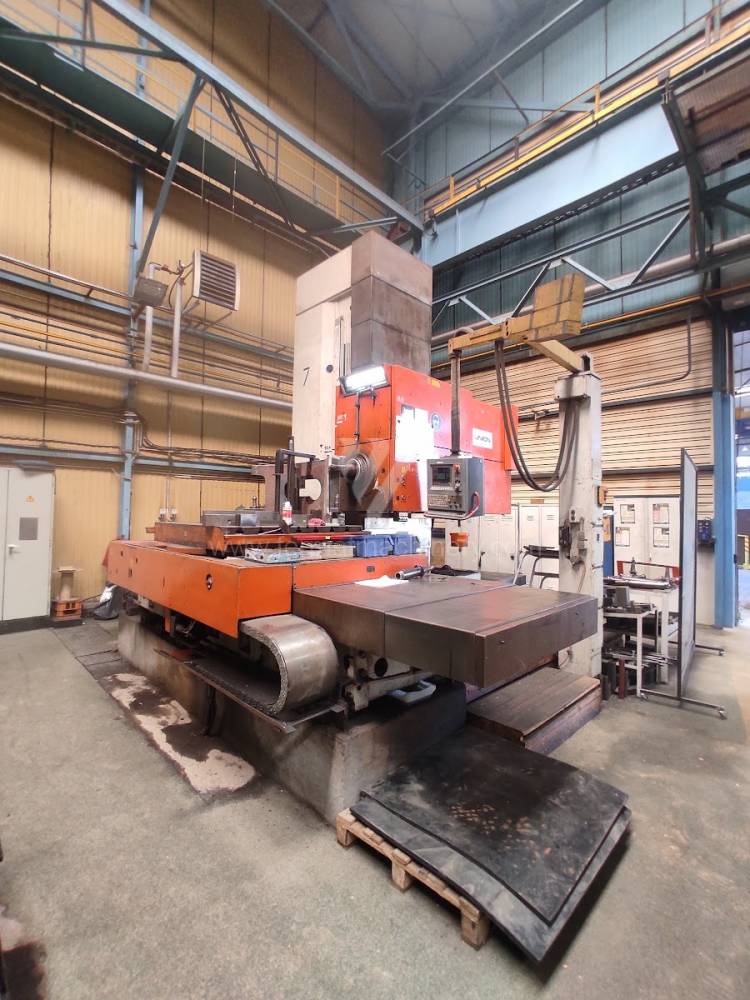 |
BFKF 150 |
251720 | UNION | 1979 | Control system Fidia: Diameter of working spindle: 150 mm Travel X-axis: 2000 mm Travel Y-axis: 1500 mm Spindle speed: 1 - 1000 /min. Cooling through spindle: NO |
|
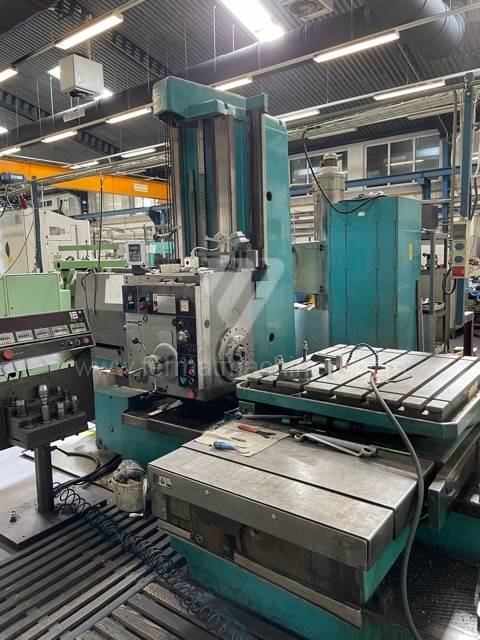 |
WHN 9 B |
251945 | TOS Varnsdorf | 1978 | Diameter of working spindle: 90 mm Travel X-axis: 1250 mm Travel Y-axis: 90 mm Spindle speed: 45 - 1120 /min. Cooling through spindle: NO Spindle travel - W axis: 680 mm |
|
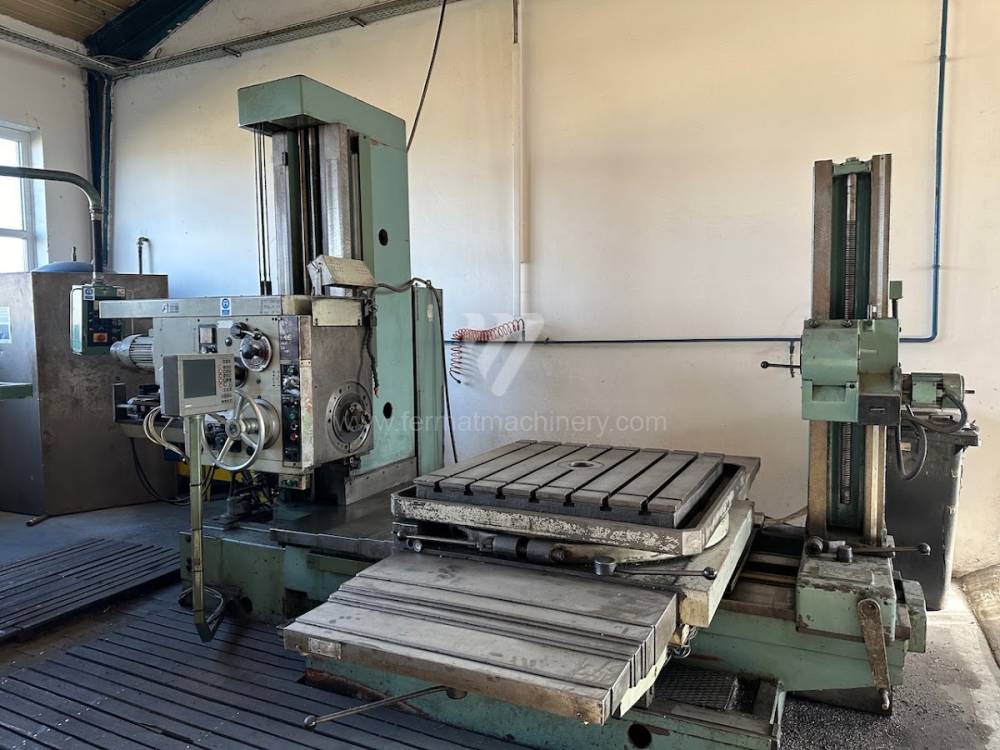 |
W 75 |
241128 | TOS Varnsdorf | 1984 | Diameter of working spindle: 75 mm Travel X-axis: 1250 mm Headstock travel (Y): 900 mm Travel Z-axis: 1000 mm Table dimensions: 950x950 mm Spindle travel - W axis: 560 mm |
|
 |
WH 10 |
251925 | TOS Varnsdorf | 1987 | Diameter of working spindle: 100 mm Travel X-axis: 1150 mm Travel Y-axis: 1000 mm Spindle speed: 0 - 1200 /min. Cooling through spindle: NO Spindle travel - W axis: 630 mm |
|
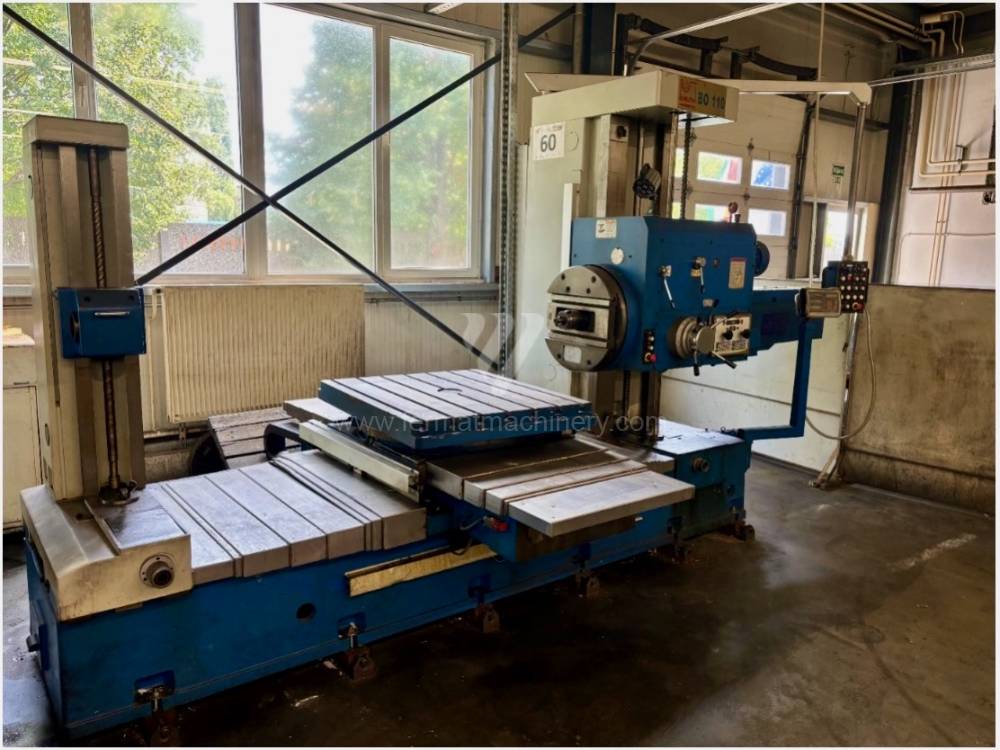 |
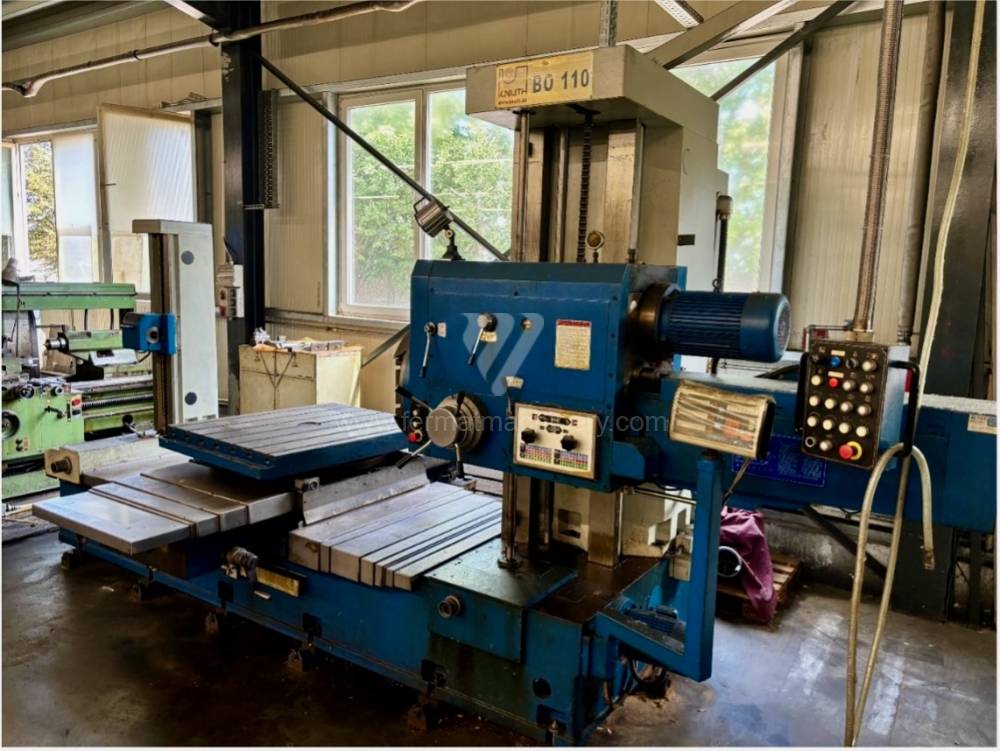
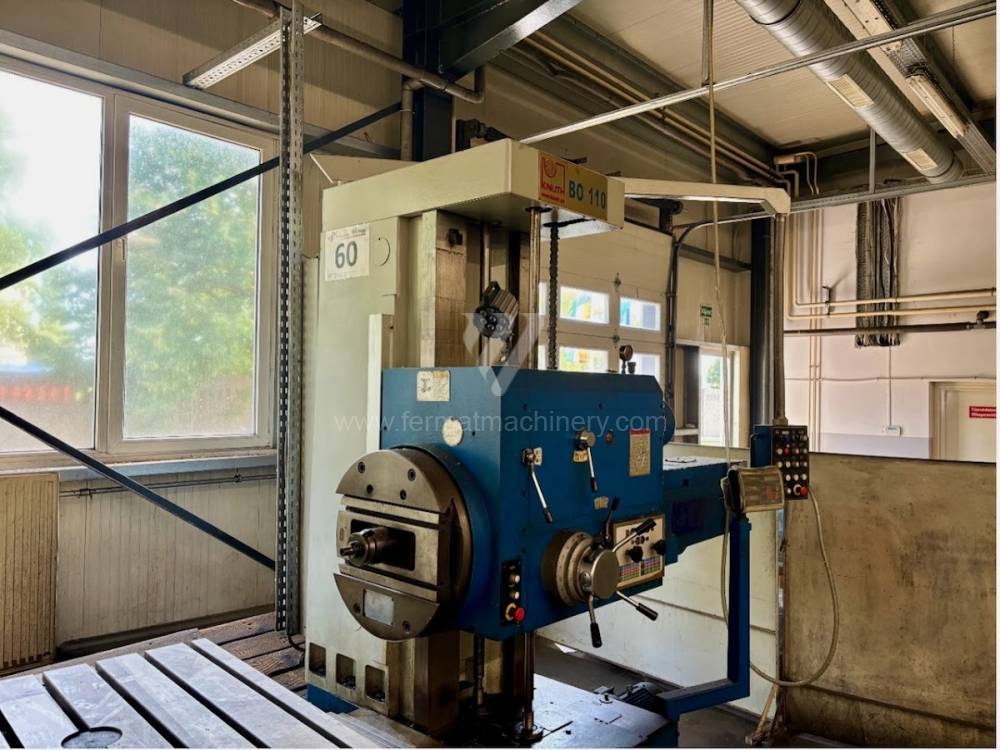
BO 110 |
241996 | KNUTH Werkzeugmaschinen GmbH | 2013 | Diameter of working spindle: 110 mm Travel X-axis: 900 mm Travel Y-axis: 900 mm Spindle speed: 8 - 1000 /min. Cooling through spindle: NO Spindle travel - W axis: 600 mm |
|
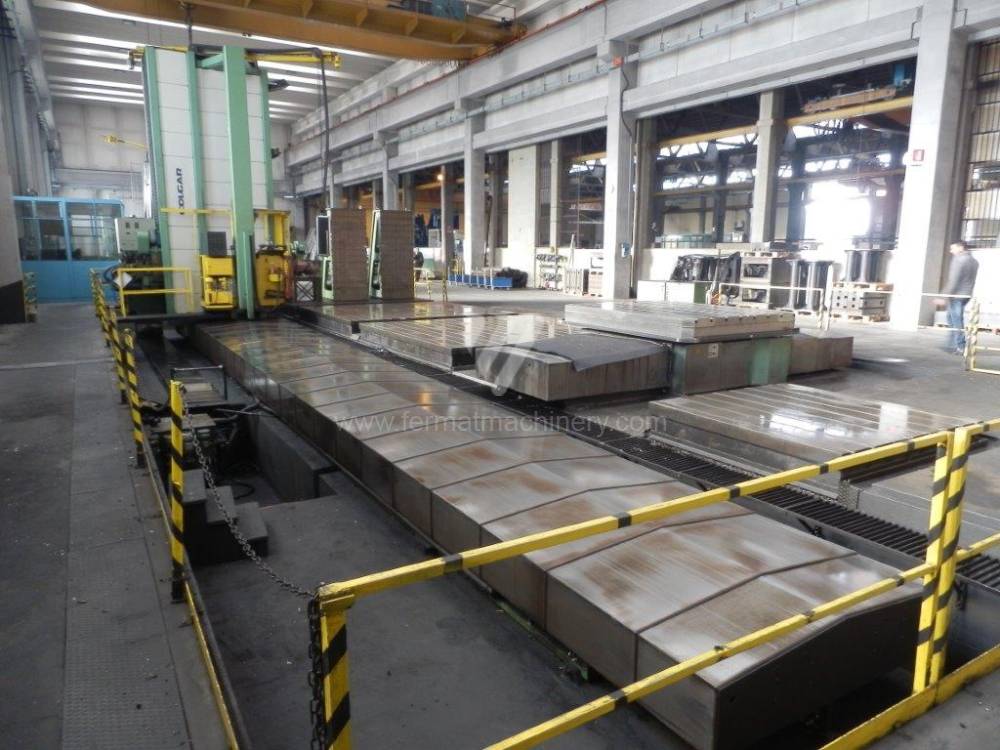 |
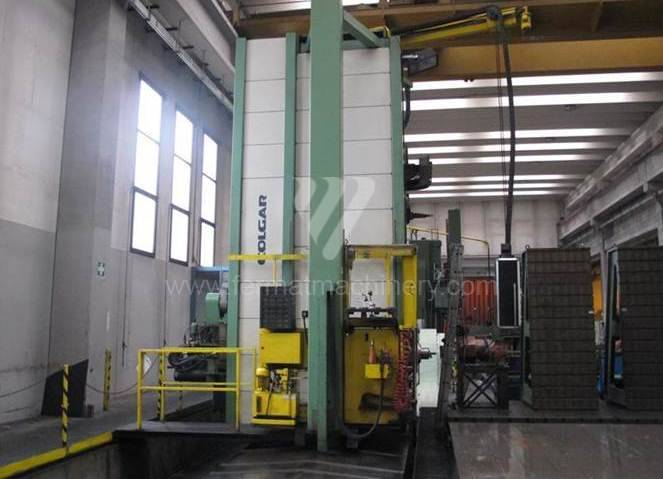
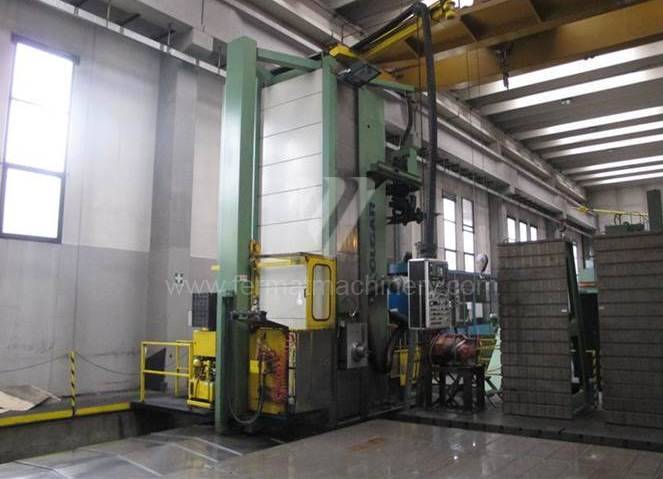
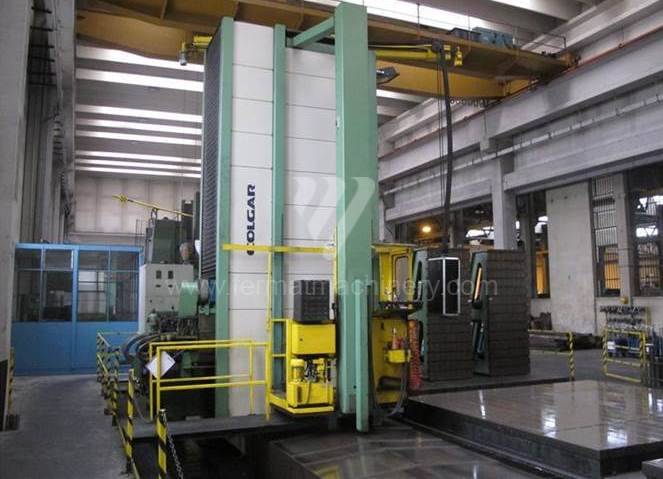
FRAL 70C16 |
241059 | Colgar International S.r.l. | 1989 | Control system ECS: Diameter of working spindle: 160 mm Travel X-axis: 15500 mm Travel Y-axis: 1000 mm Spindle speed: 0 - 1500 /min. Spindle travel - W axis: 800 mm |
|
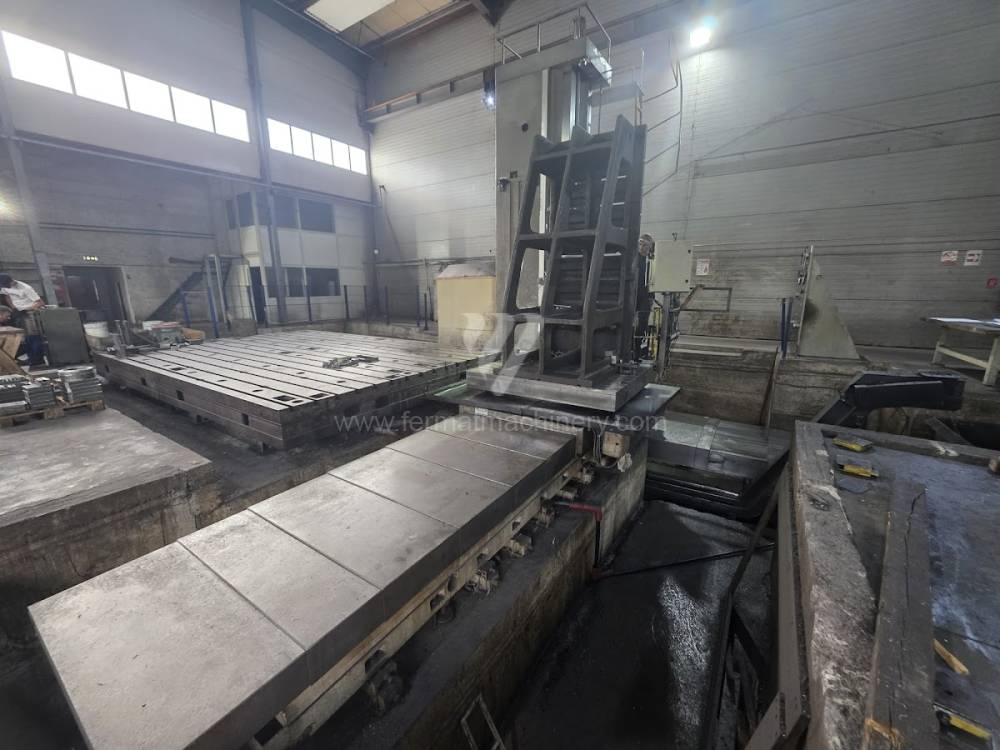 |
BMF 150 |
261725 | Titan | Control system Siemens: Sinumerik 840D Sl Diameter of working spindle: 150 mm Travel X-axis: 7800 mm Travel Y-axis: 3300 mm Spindle speed: 0 - 2600 /min. Spindle travel - W axis: 800 mm |
||
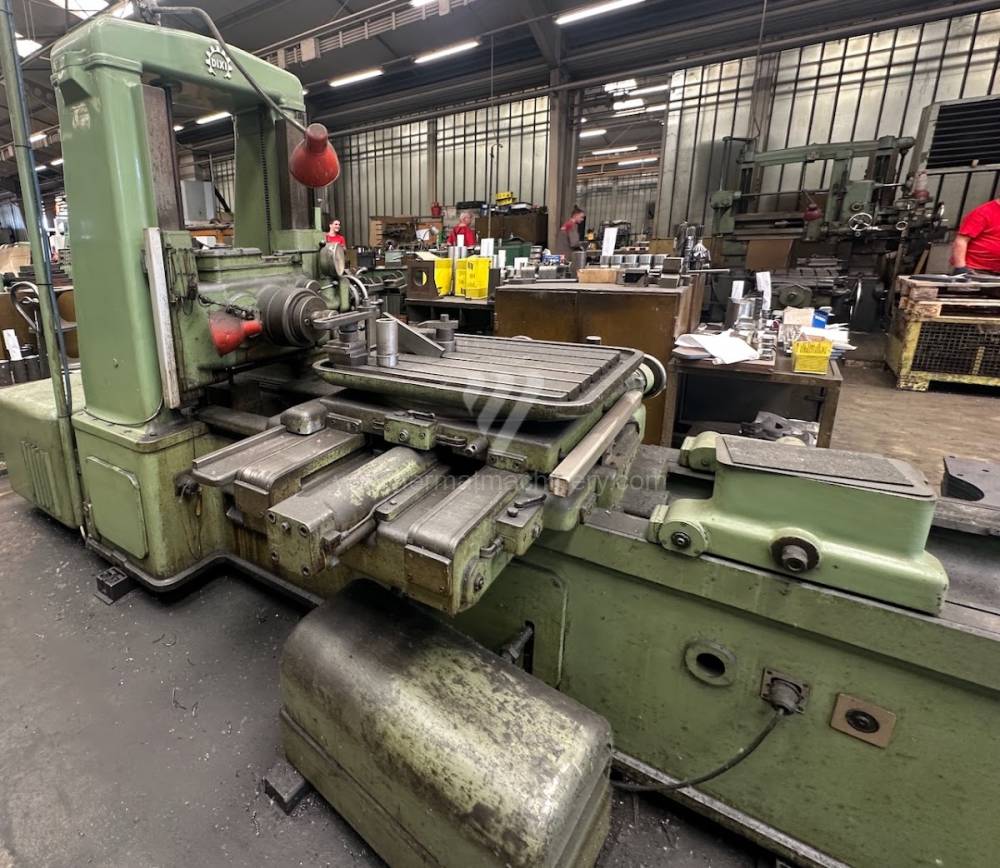 |
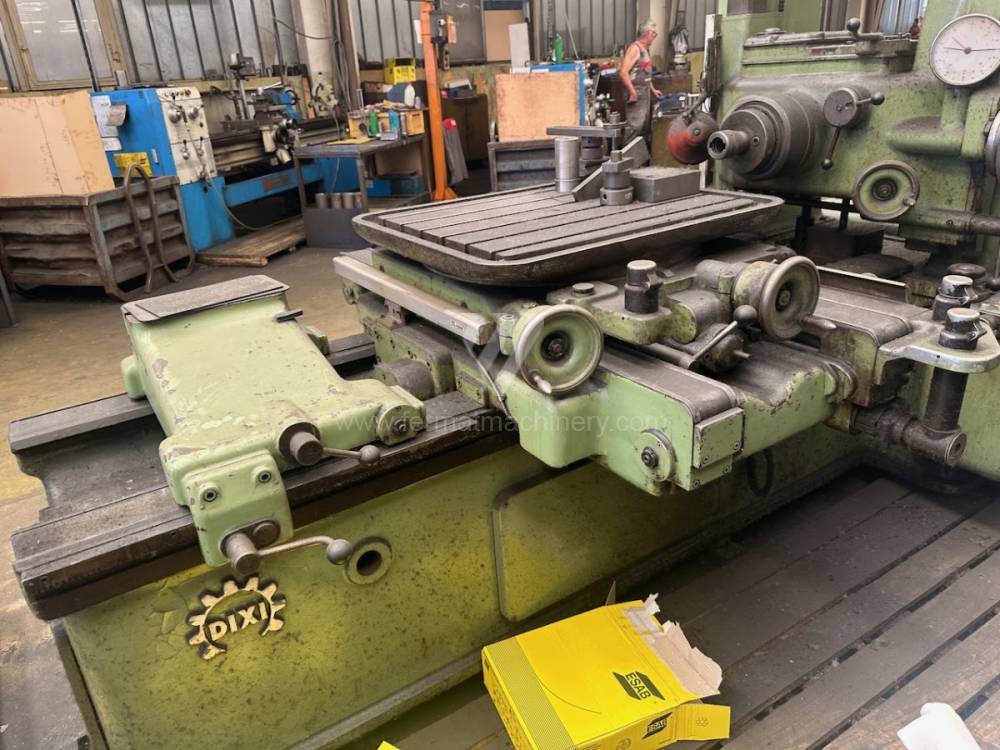
DIXI 60 |
251578 | Dixi | Diameter of working spindle: 60 mm Travel X-axis: 580 mm Travel Y-axis: 500 mm Spindle speed: 34 - 1400 /min. Cooling through spindle: NO Spindle travel - W axis: mm |
||
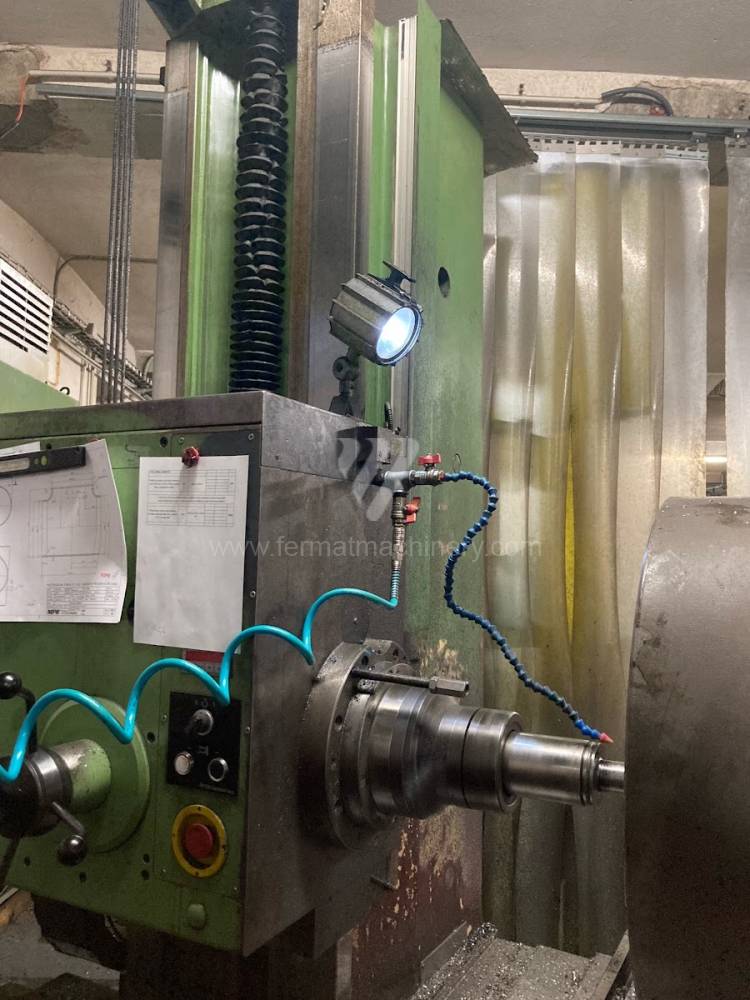 |
WH 10 CNC |
242020 | TOS Varnsdorf | 1986 | Control system Heidenhain: TNC 410 Diameter of working spindle: 100 mm Travel X-axis: 1250 mm Travel Y-axis: 1120 mm Spindle speed: 16 - 1250 /min. Cooling through spindle: NO |
|
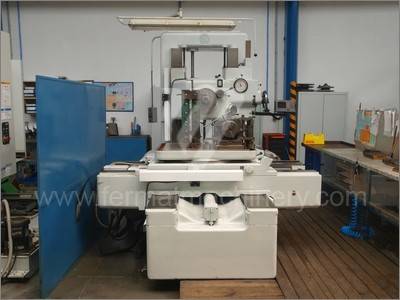 |
DIXI 75 |
251966 | Dixi | Diameter of working spindle: 75 mm Travel X-axis: 750 mm Travel Y-axis: 650 mm Spindle speed: 0 - 2800 /min. Cooling through spindle: NO Spindle travel - W axis: mm |
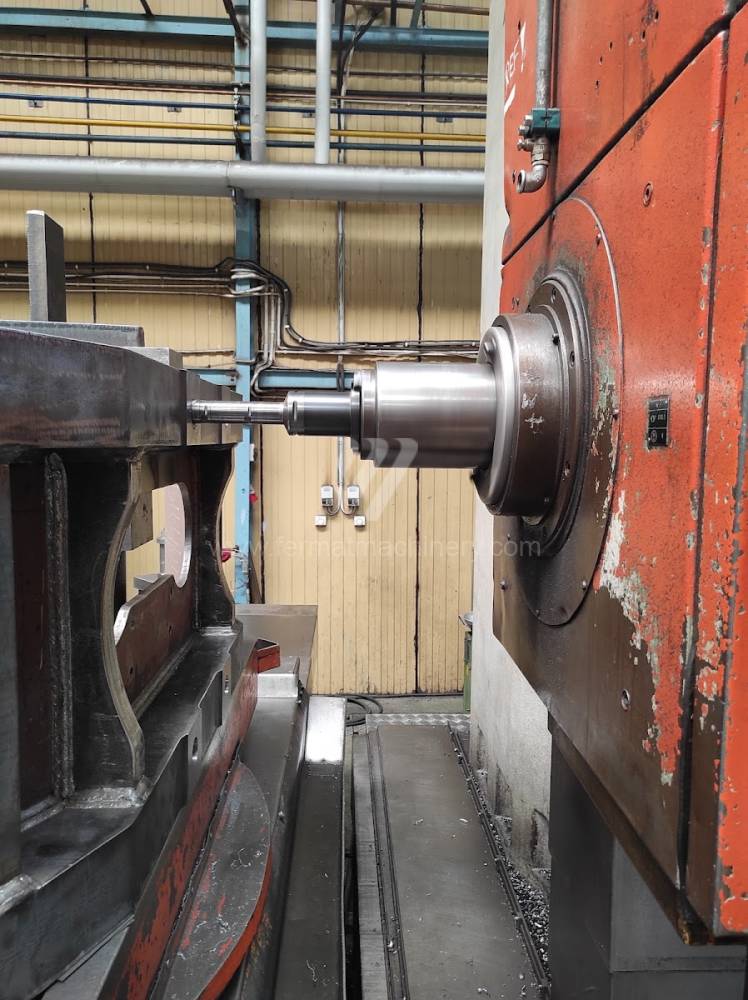
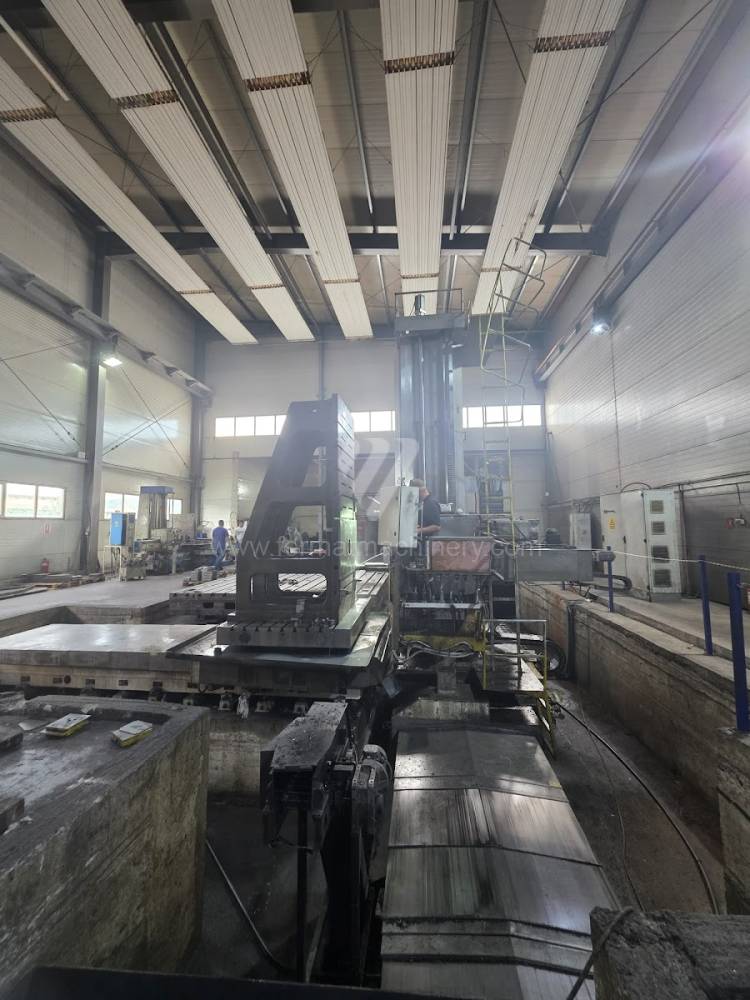
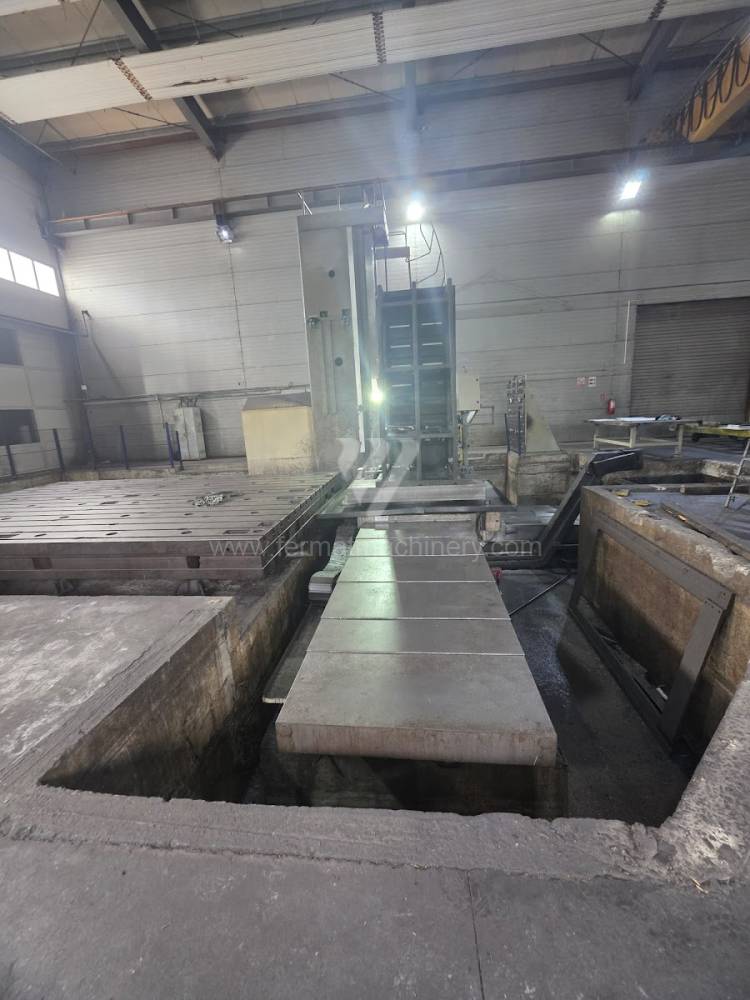
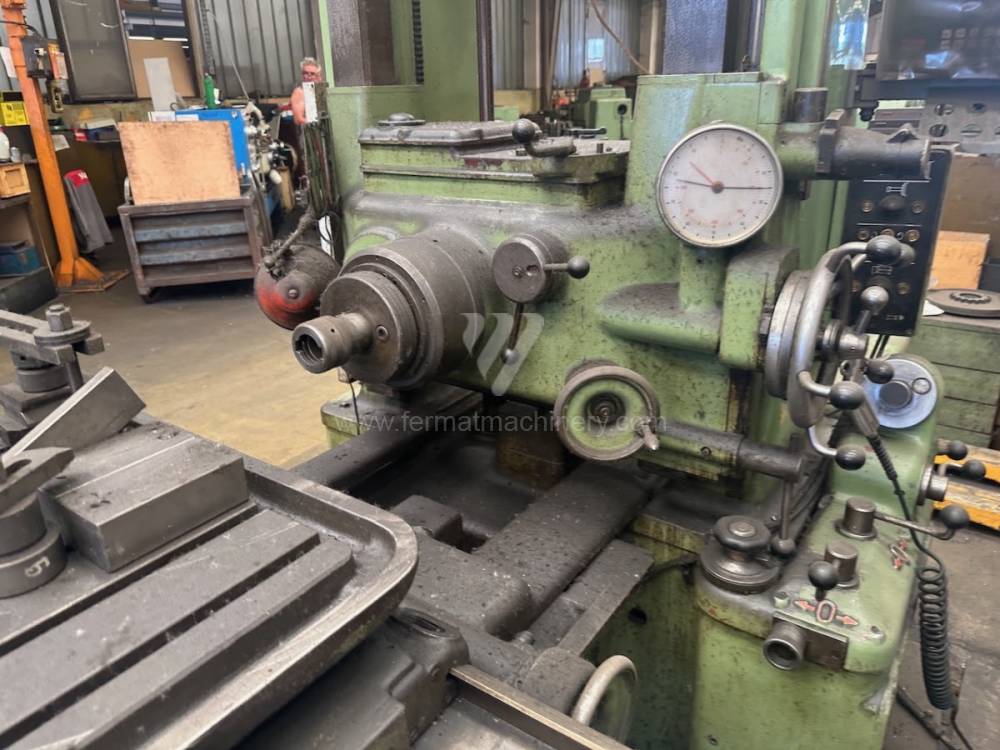
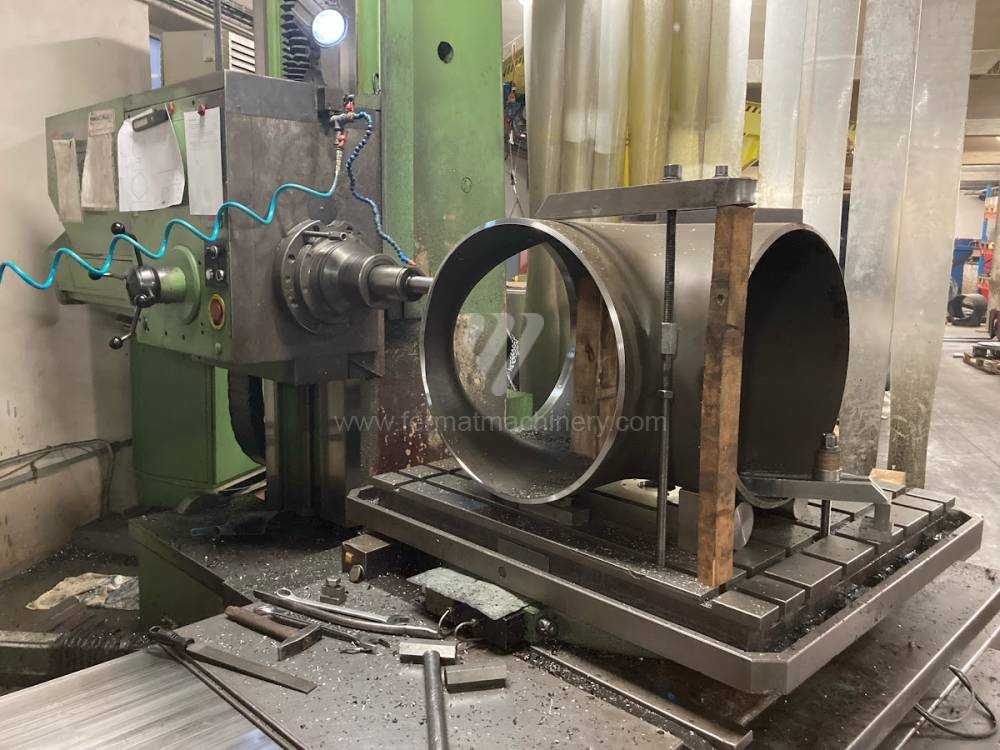
When selecting a used horizontal boring mill (such as the WFT or WFC series), the primary factors are the static and dynamic rigidity of the spindle headstock and column. The structural design of grey cast iron castings directly influences the machine's ability to damp vibrations generated during heavy-duty milling. For used FERMAT machines, emphasis is placed on the condition of the guideways—utilizing a combination of linear guideways for high dynamic movement or box-ways (sliding guideways) for maximum damping during interrupted cuts.
Spindle performance and torque are determined by the condition of the gearbox and the spindle unit bearing arrangement. Modern control systems, such as Heidenhain iTNC 640 or Fanuc 31i, allow used machines to utilize advanced adaptive feed control functions. This leads to real-time optimization of cutting forces, preventing thermal spindle deformation and extending the service life of bearing sets. Thermal stabilization, ensured by spindle cooling, is essential for horizontal boring mills to maintain dimensional stability during long boring cycles.
Acquiring a used boring mill represents a strategic investment with a significantly faster ROI (Return on Investment) compared to a new machine, thanks to lower depreciation and immediate availability. The key to profitability is minimizing non-productive time. Machines equipped with an Automatic Tool Changer (ATC) and high-capacity rotary tables (e.g., 15–20 tons) allow for complex workpiece machining in a single setup, dramatically reducing refixturing errors and increasing production throughput.
Modernizing drives and implementing digital scales (DRO) on older machine frames allows for positioning accuracy that meets the standards of demanding sectors like power generation and shipbuilding. From a long-term strategy perspective, the availability of spare parts for the kinematic chain and the ability to integrate the machine into an ERP system for OEE (Overall Equipment Effectiveness) tracking are critical.