
 Français
 L'italiano
 Magyar
 Deutsch
 Polski
 Română
 Español
 Українська
 Čeština
 Machining centres
 +420 778 547 838
 info@fermat.cz
Machining centres
| Name of a product | Inventory number | Producer | YOM | Parameters | ||
|---|---|---|---|---|---|---|
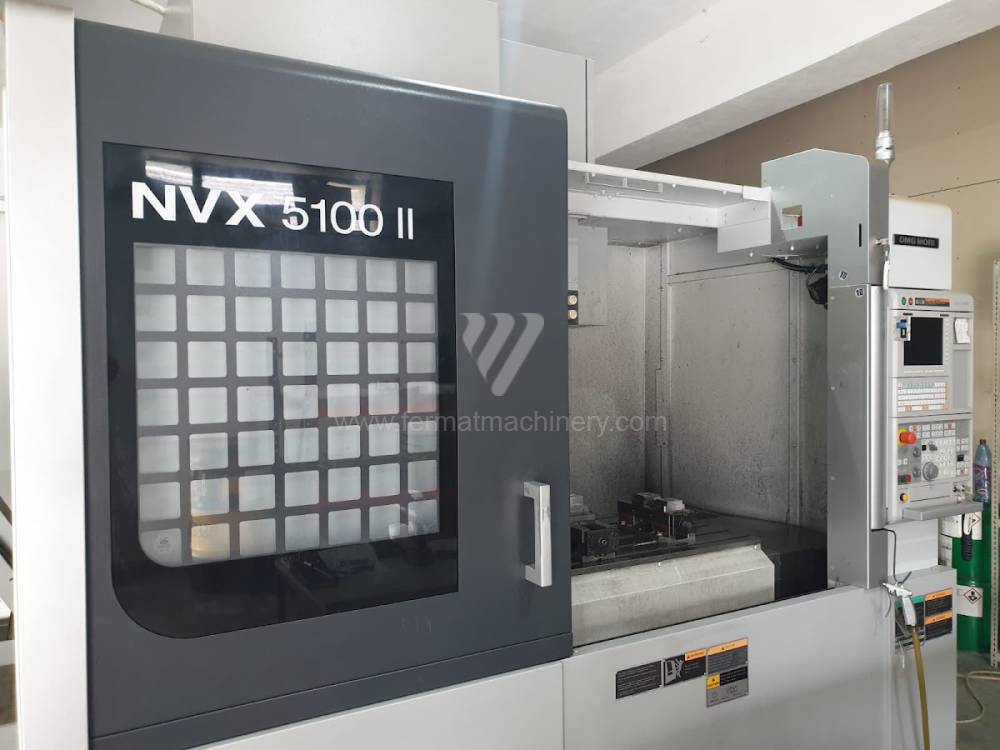 |
NVX5100 II |
241420 | MORI SEIKI | 2014 | Control system MORI SEIKI: Clamping area of table: 1350 × 600 mm Travel X-axis: 1050 mm Travel Y-axis: 530 mm Travel Z-axis: 510 mm Spindle speed: 0 - 20000 /min. |
|
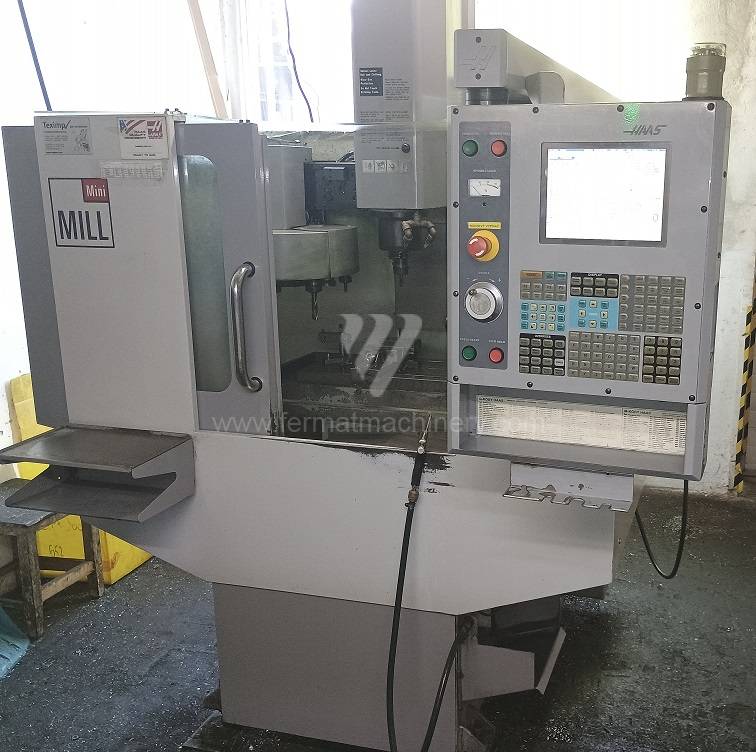 |
MiniMill HE |
251988 | Haas Automation | 2006 | Control system Haas: Clamping area of table: 305 x 914 mm Travel X-axis: 406 mm Travel Y-axis: 356 mm Travel Z-axis: 381 mm Spindle speed: 0 - 6000 /min. |
|
 |
MCV 500 |
251978 | KOVOSVIT MAS, a.s. | 1999 | Control system Heidenhain: TNC 407 Clamping area of table: 800x500 mm Travel X-axis: 500 mm Travel Y-axis: 500 mm Travel Z-axis: 500 mm Spindle speed: 0 - 8000 /min. |
|
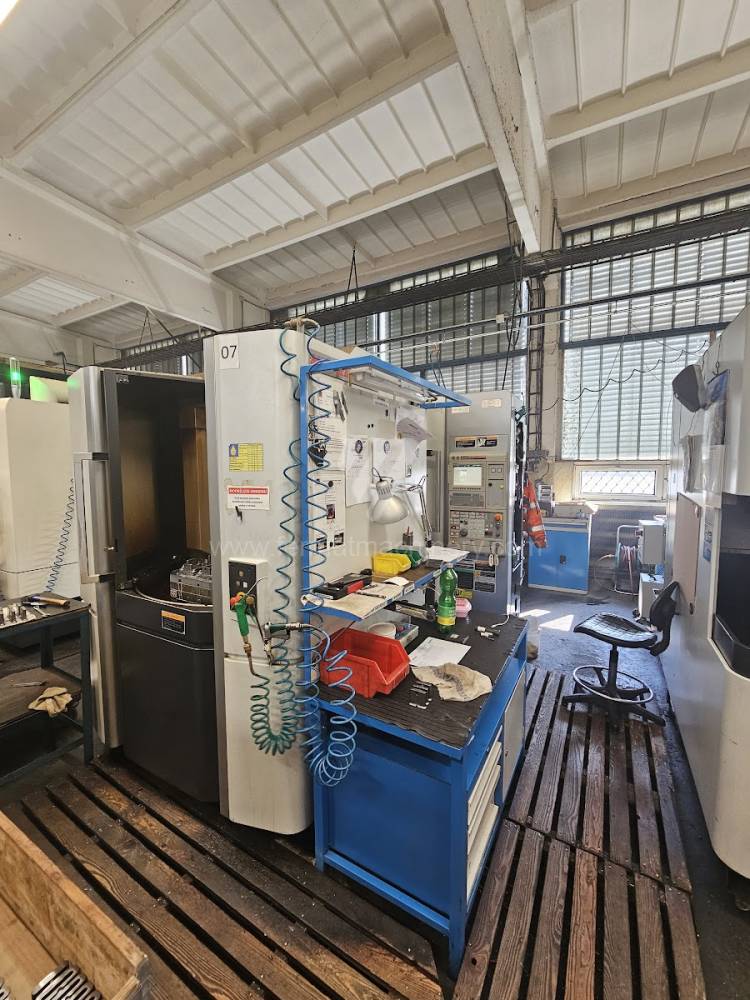 |
NHX 4000 |
251142 | DMG MORI | 2012 | Clamping area of table: 400 x 400 mm Travel X-axis: 560 mm Travel Y-axis: 560 mm Travel Z-axis: 660 mm Spindle speed: 1 - 12000 /min. Number of driven axes: 4 |
|
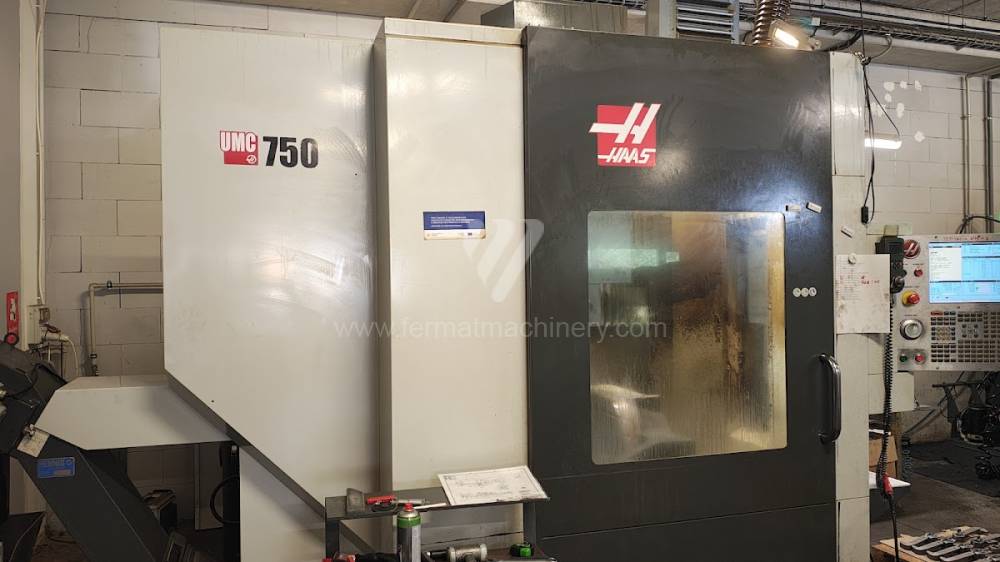 |
UMC - 750 |
261702 | Haas Automation | 2014 | Control system Haas: Clamping area of table: 630x500 mm Travel X-axis: 762 mm Travel Y-axis: 508 mm Travel Z-axis: 508 mm Spindle speed: 0 - 12000 /min. |
|
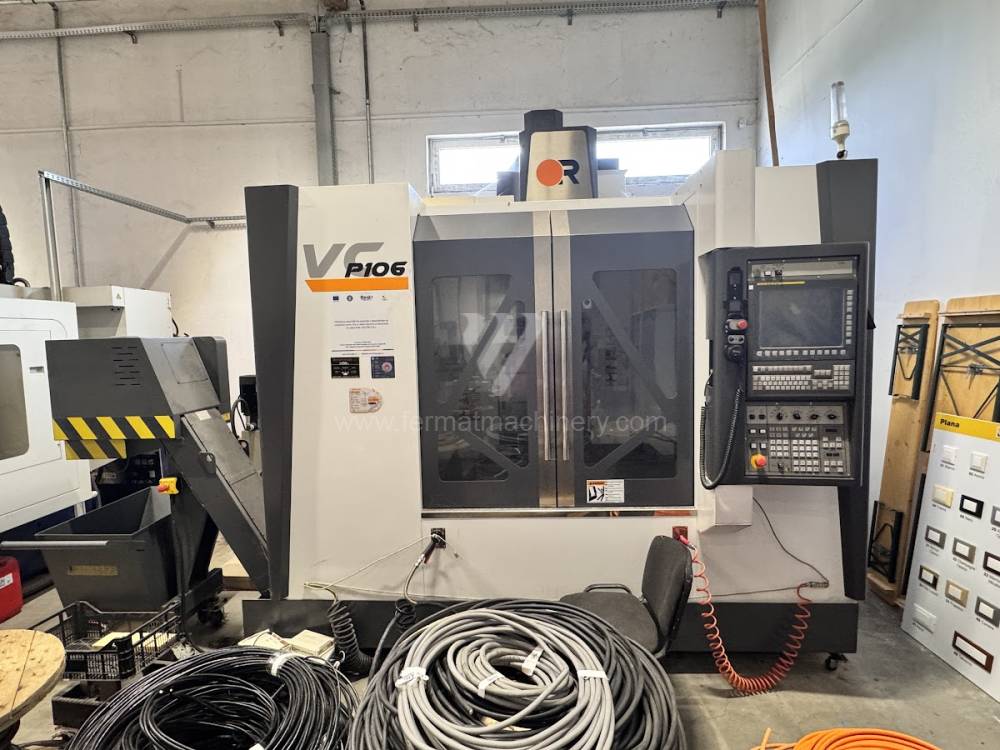 |
Vcenter P106 |
261400 | Victor Machinery Solutions | 2018 | Control system Fanuc: 0i-MF Clamping area of table: 1120x520 mm Travel X-axis: 1060 mm Travel Y-axis: 600 mm Travel Z-axis: 560 mm Spindle speed: 0 - 12000 /min. |
|
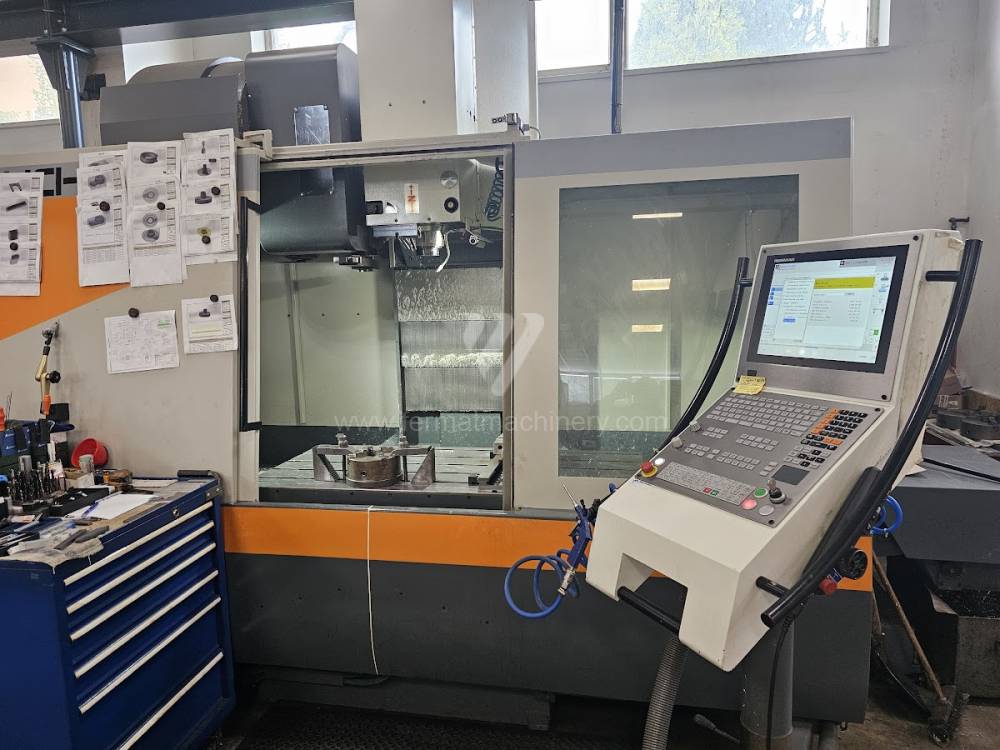 |
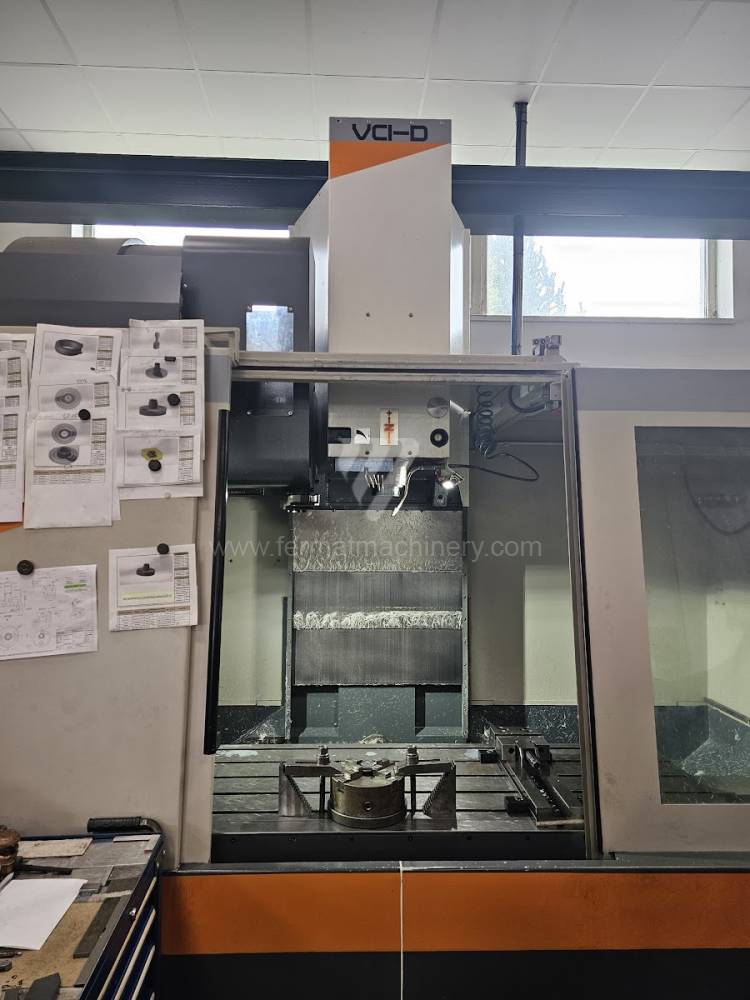
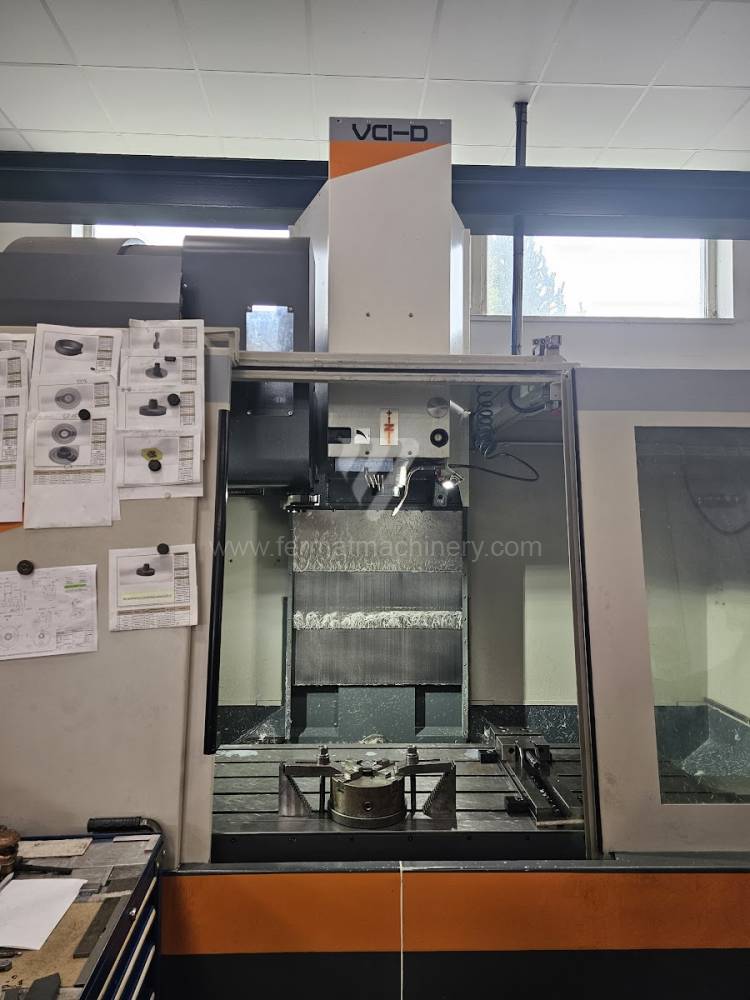
VCI-D 1270 |
241865 | KOVOSVIT MAS, a.s. | 2002 | Control system Heidenhain: TNC 620 Clamping area of table: 1500x670 mm Travel X-axis: 1270 mm Travel Y-axis: 610 mm Travel Z-axis: 720 mm Spindle speed: 20 - 12000 /min. |
|
 |
DMC 635 V ecoline |
261572 | DMG MORI | 2016 | Control system Siemens: Sinumerik 810 Clamping area of table: 790 x 560 mm Travel X-axis: 635 mm Travel Y-axis: 510 mm Travel Z-axis: 460 mm Spindle speed: 0 - 8000 /min. |
|
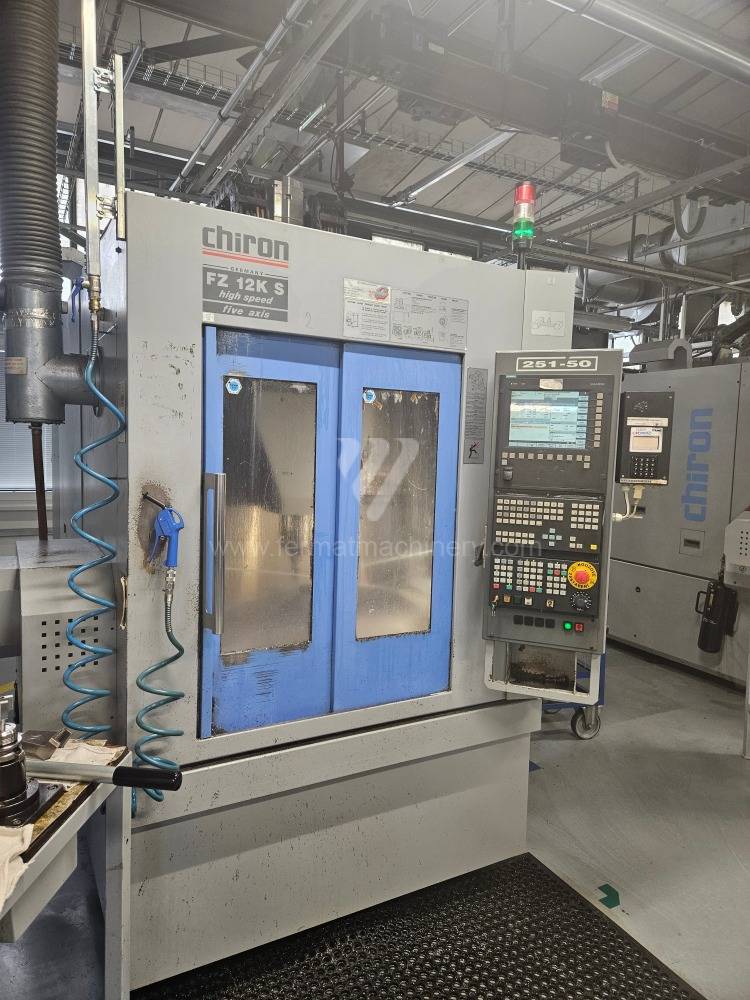 |
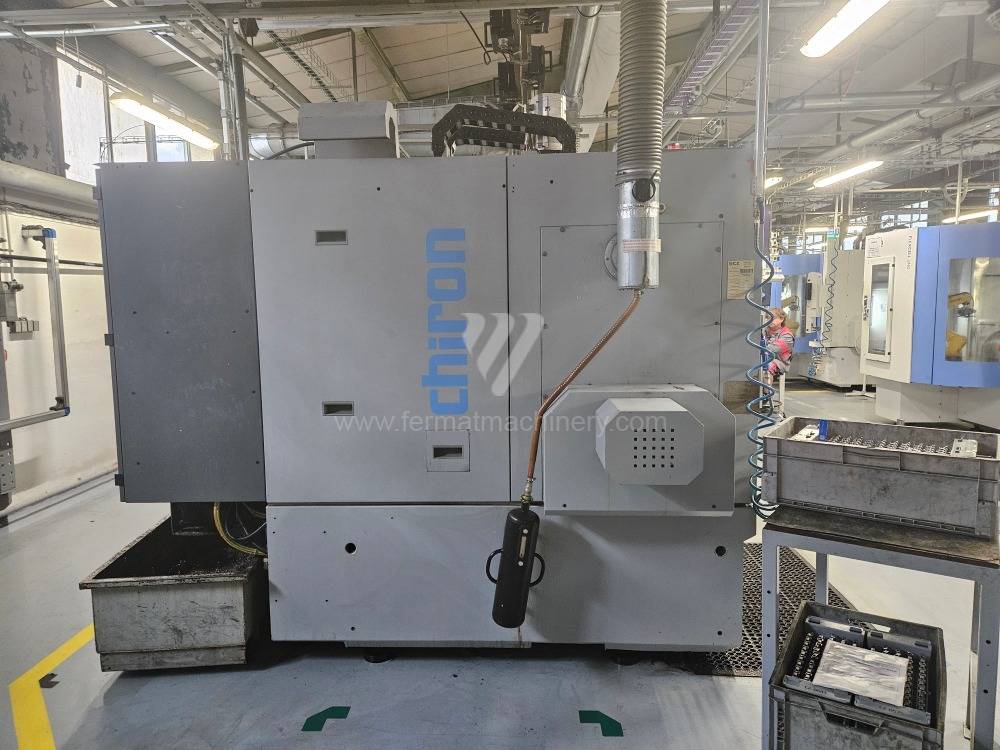
FZ 12K S |
261442 | Chiron | 2008 | Control system Siemens: Clamping area of table: mm Travel X-axis: 550 mm Travel Y-axis: 400 mm Travel Z-axis: 360-400 mm Spindle speed: 0 - 15000 /min. |
|
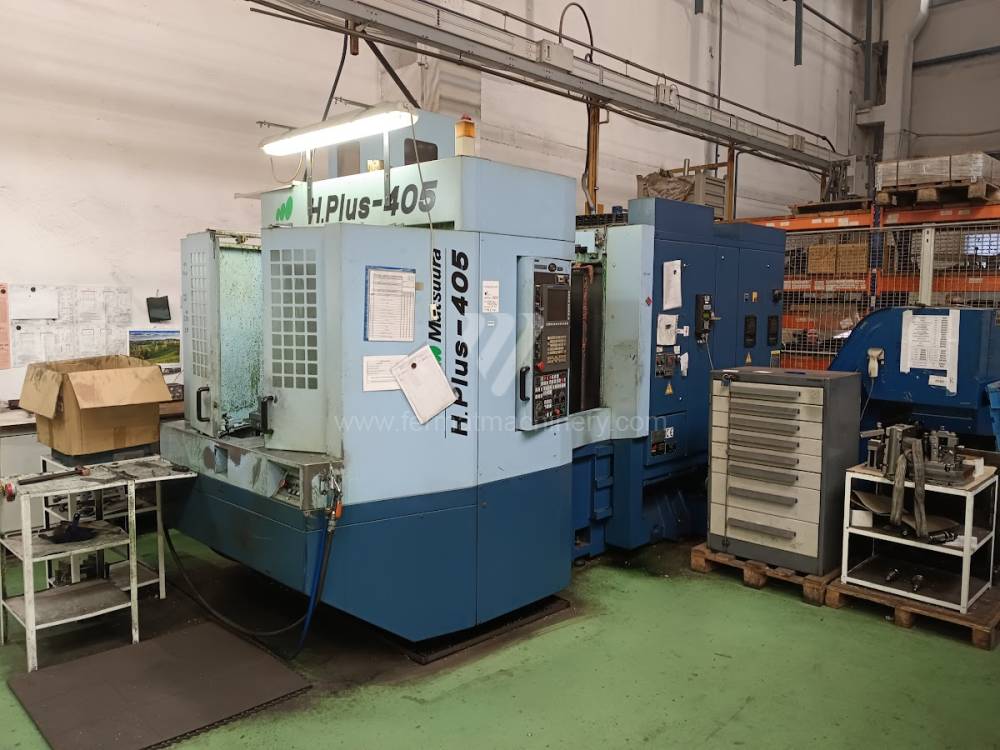 |
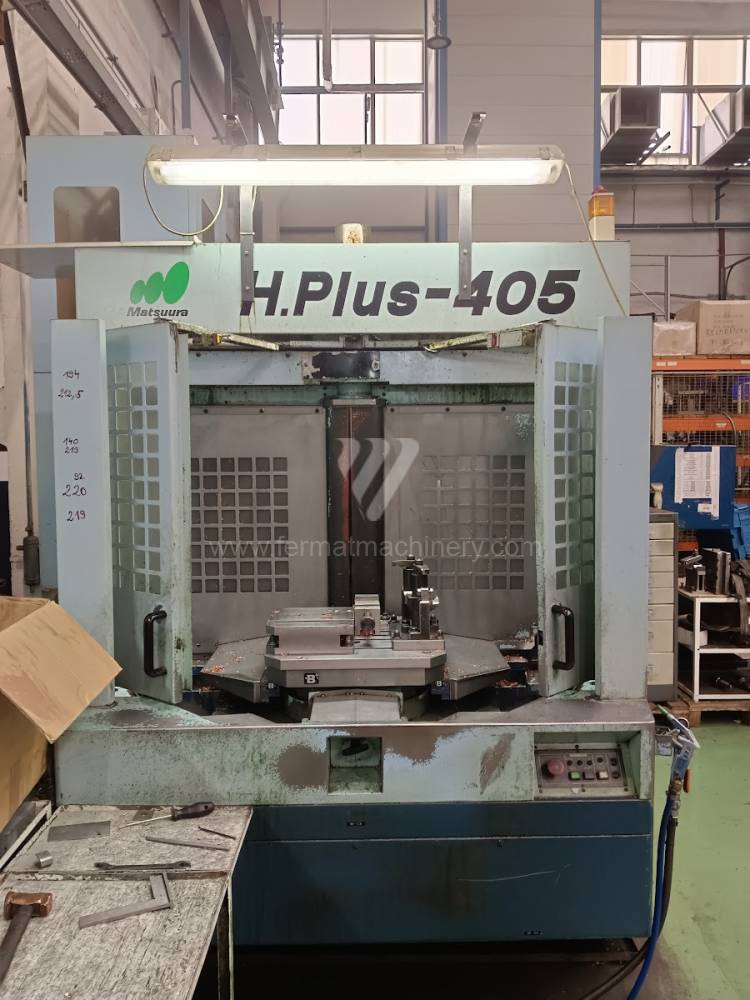
H.Plus-405 |
251975 | Matsuura | 2008 | Clamping area of table: 500x500 mm Travel X-axis: 660 mm Travel Y-axis: 660 mm Travel Z-axis: 660 mm Spindle speed: 10 - 12000 /min. Number of driven axes: 4 |
|
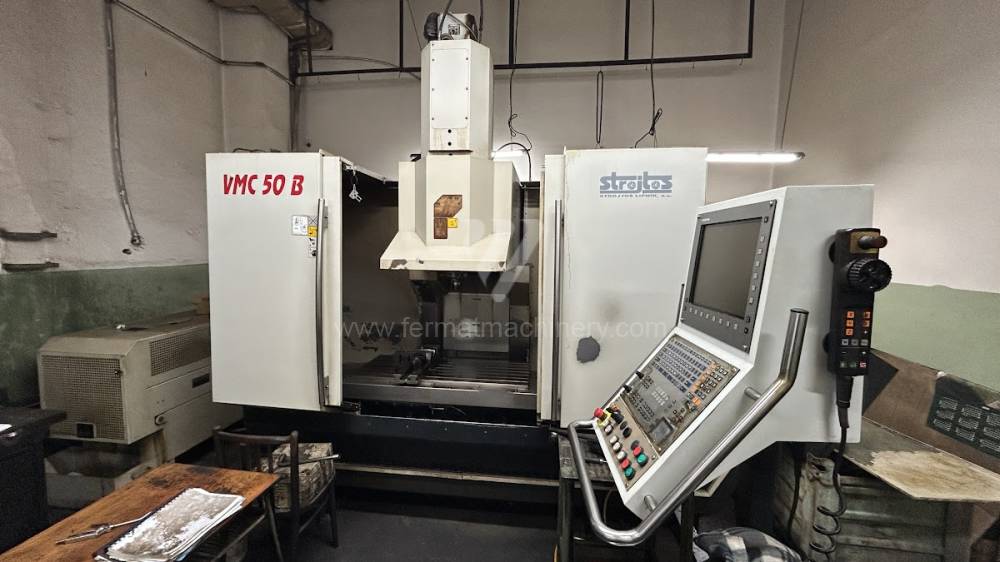 |
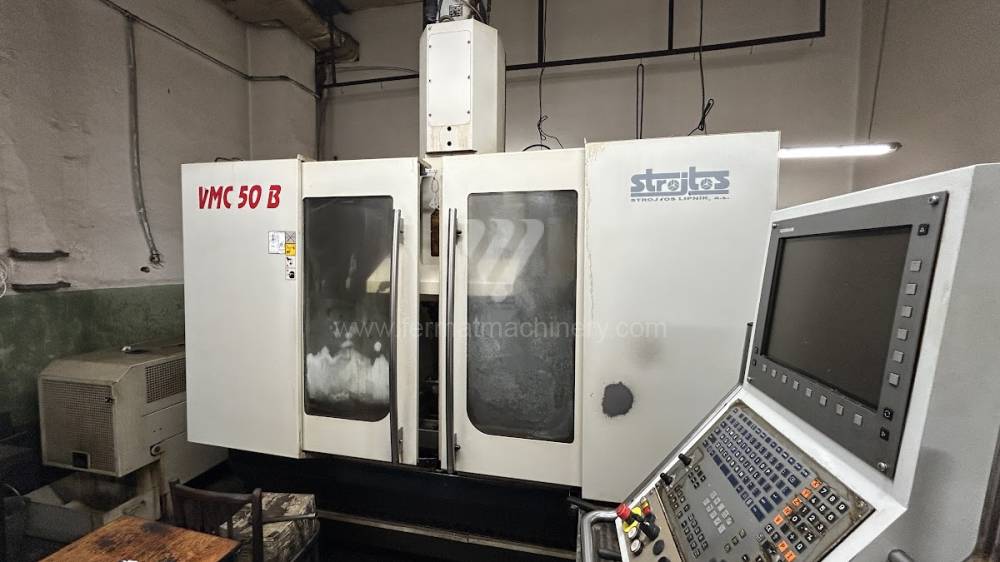
VMC 50 B |
261676 | Strojtos | 2008 | Control system Heidenhain: TNC 530 Clamping area of table: 500x1000 mm Travel X-axis: 1000 mm Travel Y-axis: 500 mm Travel Z-axis: 500 mm Spindle speed: 0 - 10000 /min. |
|
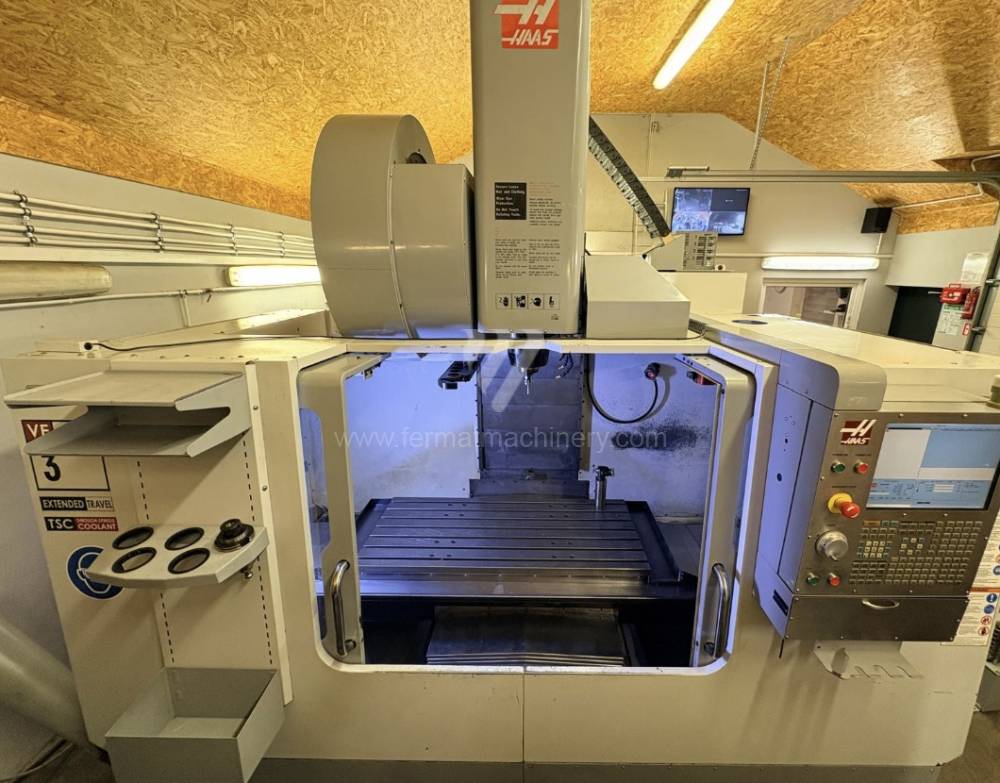 |
VF-3YT/50 |
261695 | Haas Automation | 2008 | Control system Haas: Clamping area of table: 1372x610 mm Travel X-axis: 1016 mm Travel Y-axis: 660 mm Travel Z-axis: 635 mm Spindle speed: 0 - 7500 /min. |
|
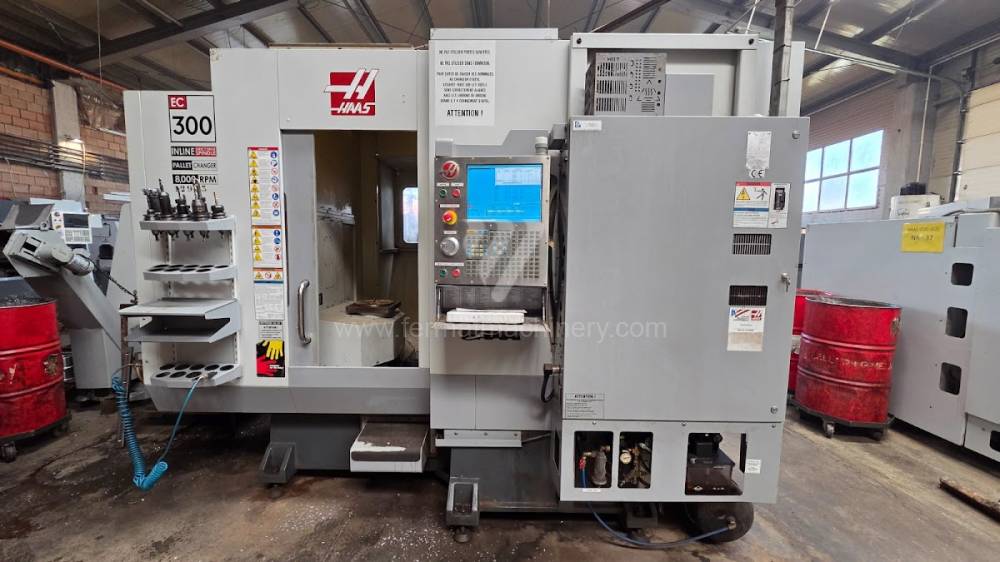 |
HAAS EC-300 |
261606 | Haas Automation | 2010 | Control system Haas: Clamping area of table: 300 x 300 mm Travel X-axis: 508 mm Travel Y-axis: 457 mm Travel Z-axis: 356 mm Spindle speed: 8000 - /min. |
|
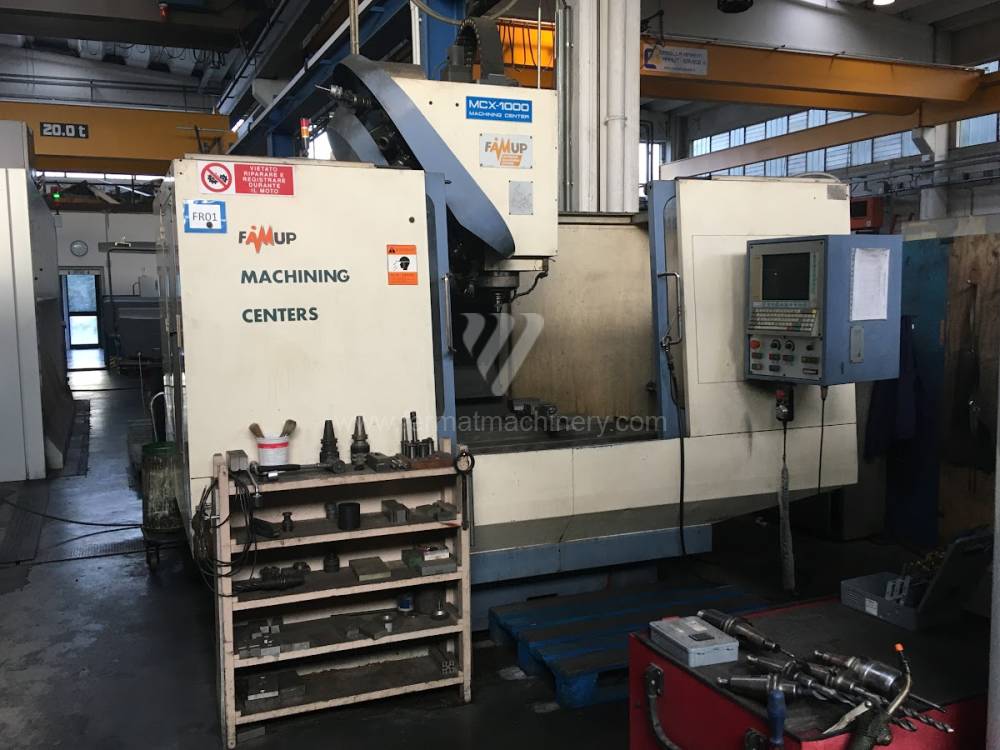 |
MCX 1000 |
241203 | FAMUP | 1994 | Control system Selca: 3045 Clamping area of table: mm Travel X-axis: 1000 mm Travel Y-axis: 500 mm Travel Z-axis: 350 mm Spindle speed: 0 - 4000 /min. |
|
 |
Power Speed 4000 |
261646 | SHW Werkzeugmaschinen | 2022 | Control system Heidenhain: TNC 640 Clamping area of table: 2000x2000 mm Travel X-axis: 4000 mm Travel Y-axis: 2000 mm Travel Z-axis: 1600 mm Spindle speed: 0 - 8000 /min. |
|
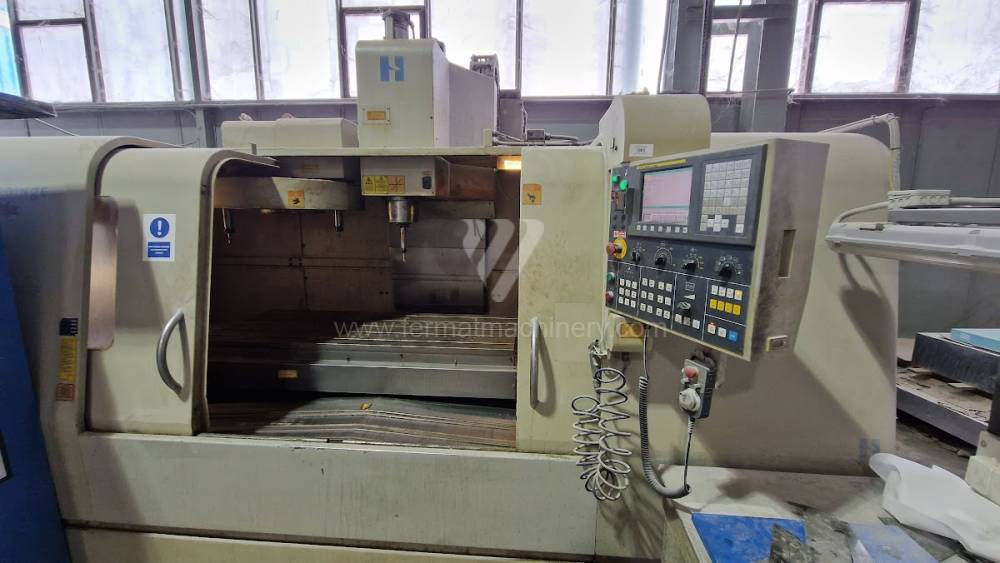 |
VMC 1500P3 - CNC |
231777 | Hardinge Inc. | 2007 | Control system Fanuc: 0i - MC Clamping area of table: 1624 x 660 mm Travel X-axis: 1524 mm Travel Y-axis: 660 mm Travel Z-axis: 635 mm Spindle speed: 0 - 8000 /min. |
|
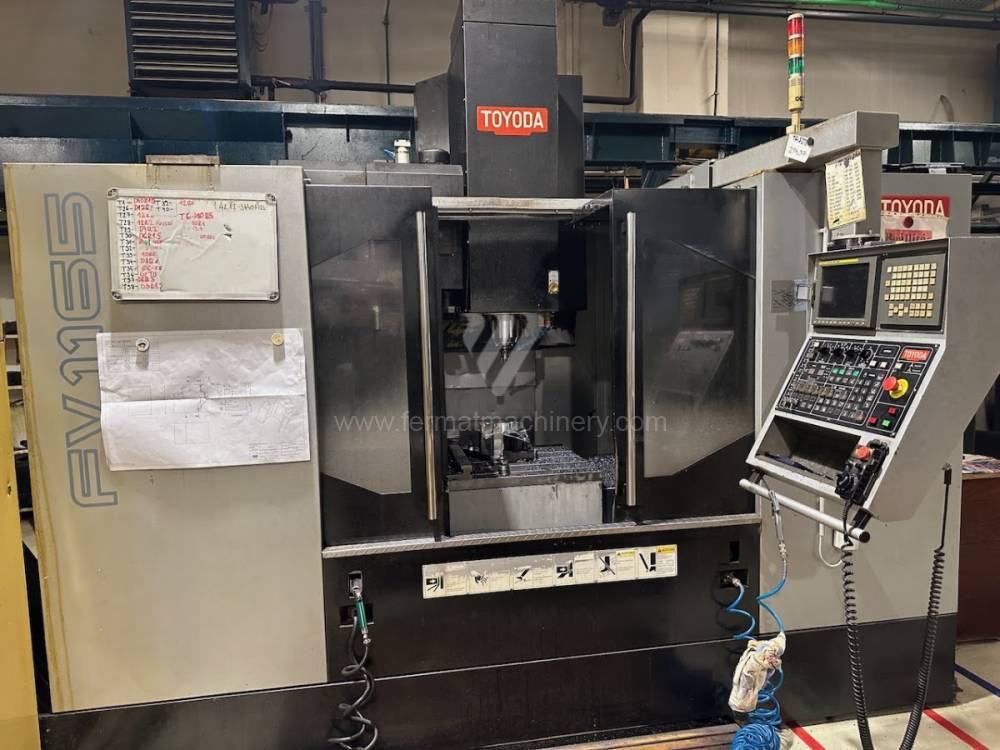 |
FV 1165 |
242039 | Toyoda | 2008 | Control system Fanuc: 18i - MB Clamping area of table: 1300x650 mm Travel X-axis: 1100 mm Travel Y-axis: 650 mm Travel Z-axis: 600 mm Spindle speed: 1 - 12000 /min. |
|
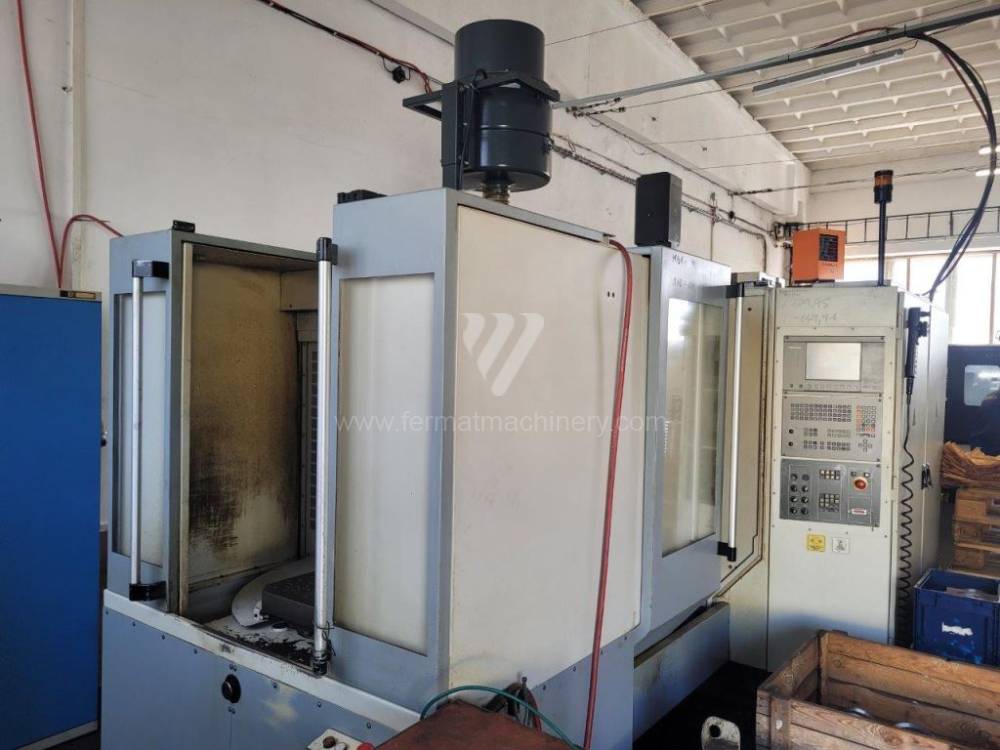 |
H 40 |
251791 | TAJMAC-ZPS, a.s. | 2004 | Control system Heidenhain: TNC 530 Clamping area of table: 400x400 mm Travel X-axis: 560 mm Travel Y-axis: 510 mm Travel Z-axis: 560 mm Spindle speed: 10 - 10000 /min. |
|
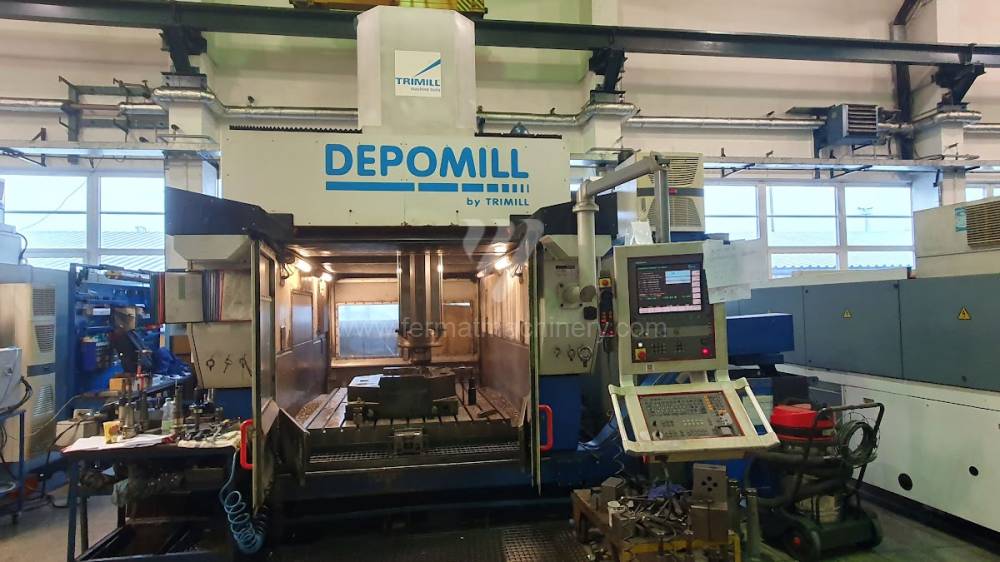 |
Depomill CUT 2012 |
261216 | TRIMILL | 2006 | Control system Heidenhain: TNC 530 Clamping area of table: 2300 x 1600 mm Travel X-axis: 2300 mm Travel Y-axis: 1200 mm Travel Z-axis: 800 mm Spindle speed: 30 - 12000 /min. |
|
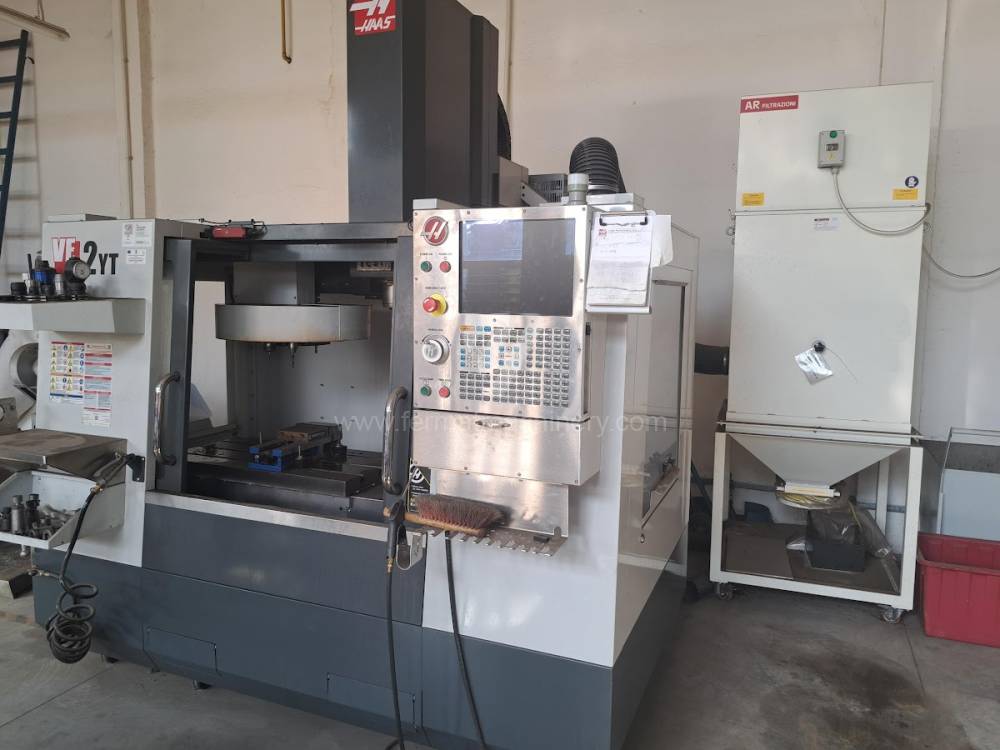 |
VF 2 |
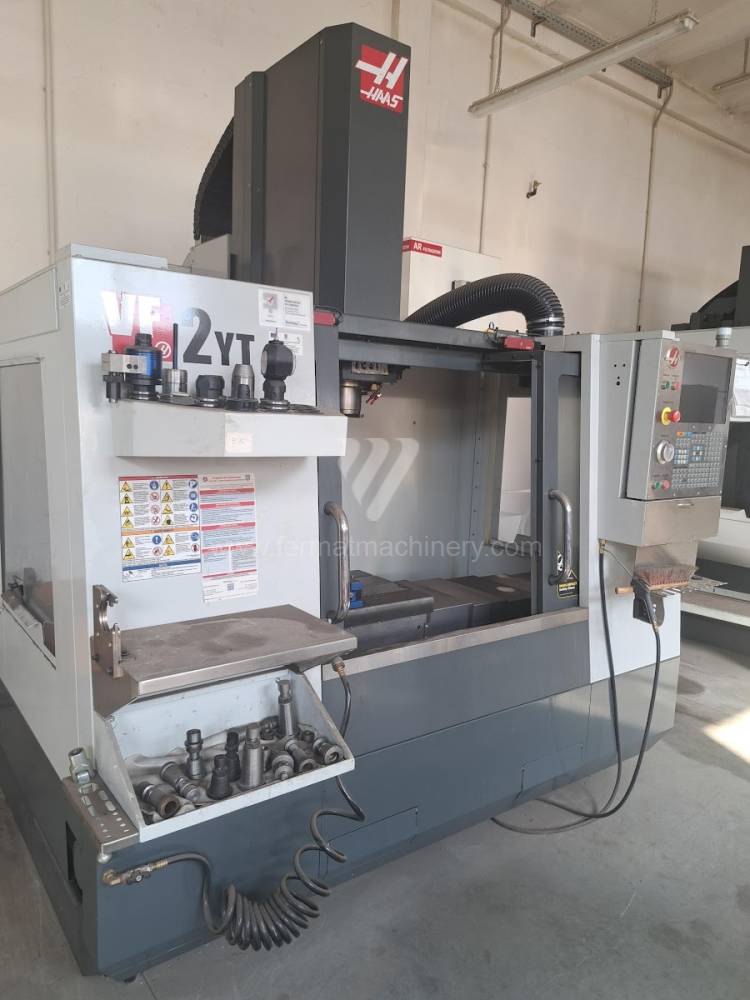
261304 | Haas Automation | 2015 | Control system Haas: Clamping area of table: 914 x 356 mm Travel X-axis: 762 mm Travel Y-axis: 406 mm Travel Z-axis: 508 mm Spindle speed: 1 - 8100 /min. |
|
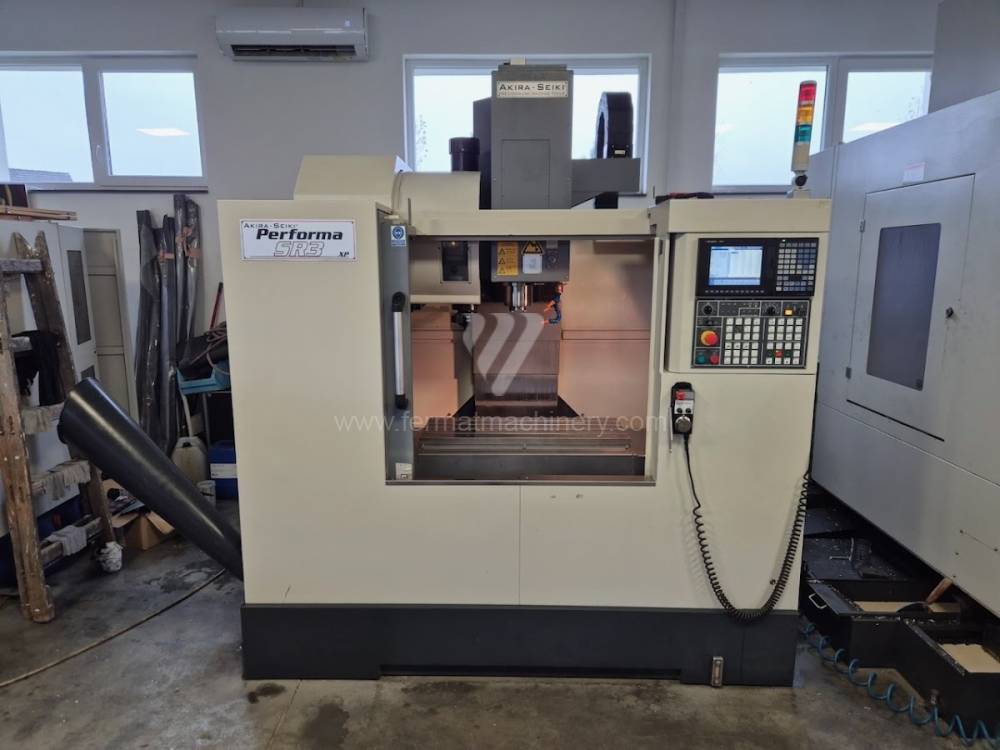 |
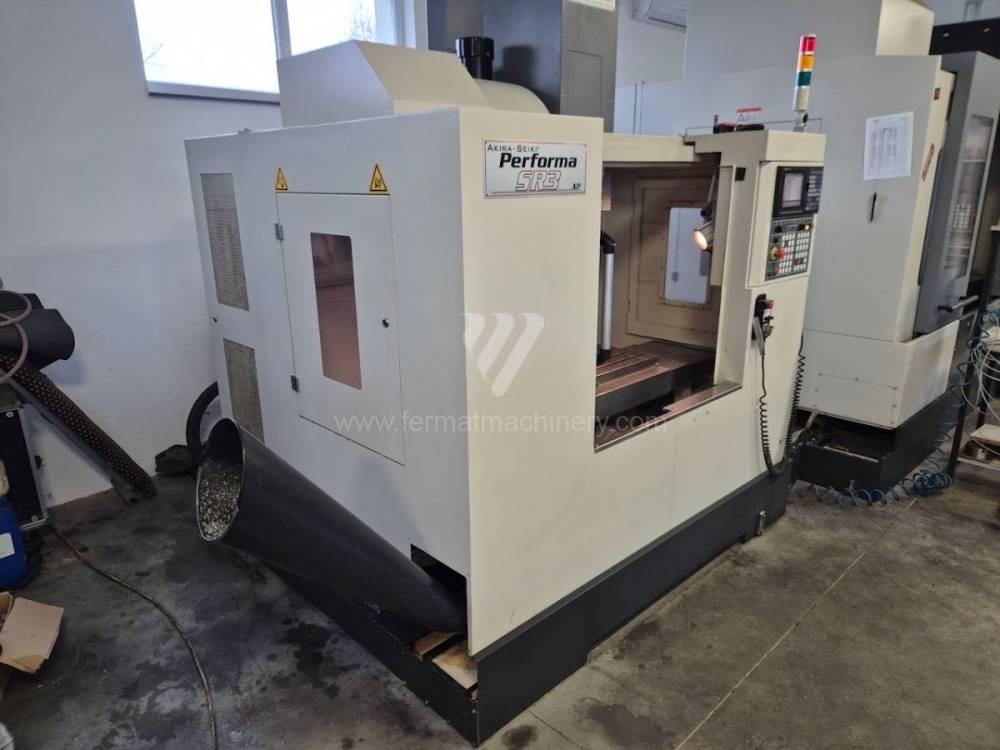
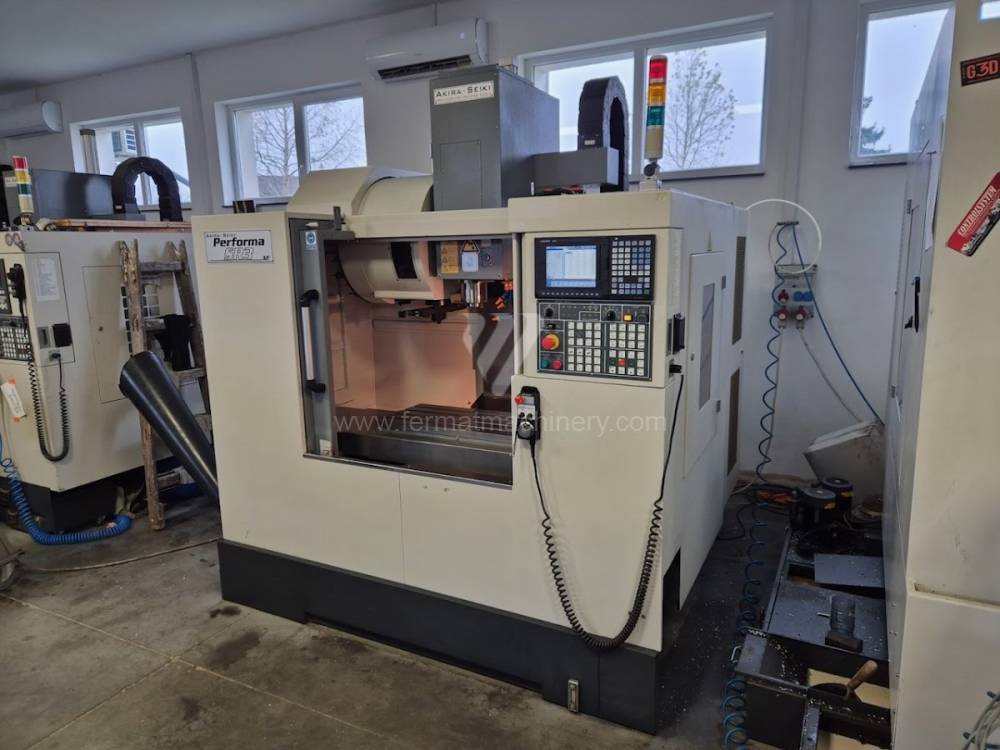
SR3 XP |
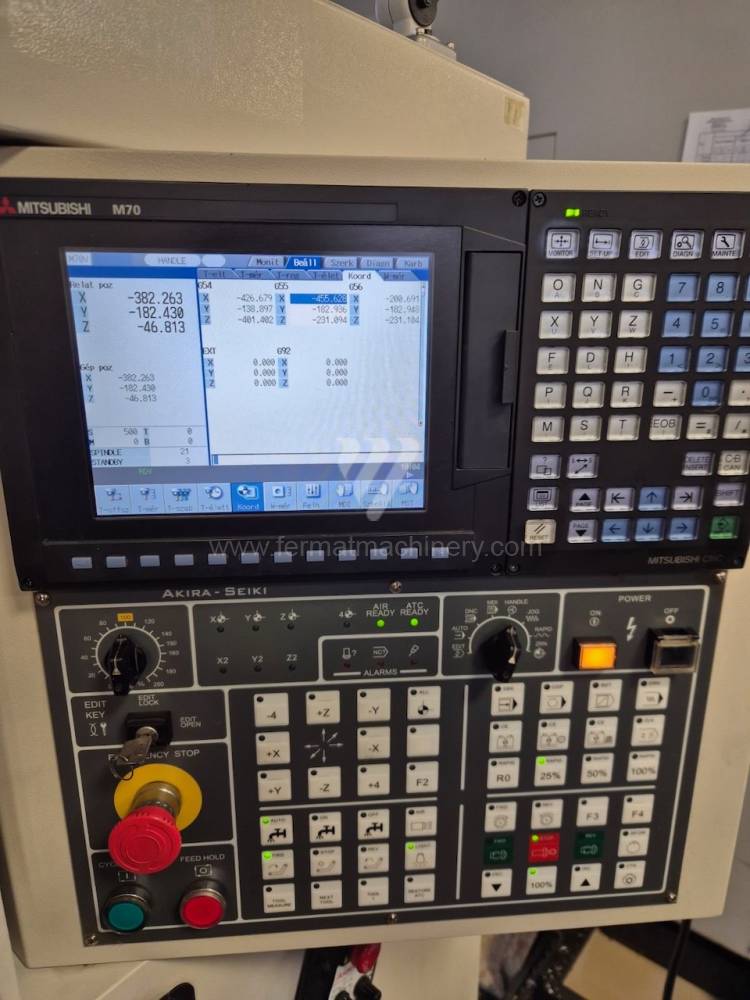
261004 | Akira Seiki | 2013 | Control system Mitsubishi: M 70 Clamping area of table: 910x380 mm Travel X-axis: 762 mm Travel Y-axis: 410 mm Travel Z-axis: 460 mm Spindle speed: 0 - 11000 /min. |
|
 |
VZ 750 |
261544 | KOVOSVIT MAS, a.s. | 2005 | Control system Heidenhain: TNC 530 Dimensions of table working surface: 1000x640 mm Spindle taper: ISO 40 . Machine dimensions l x w x h: 4500x2300x2700 mm Machine weight: 5 000 kg Rotations of clamping plate: 20 - 13000 /min |
|
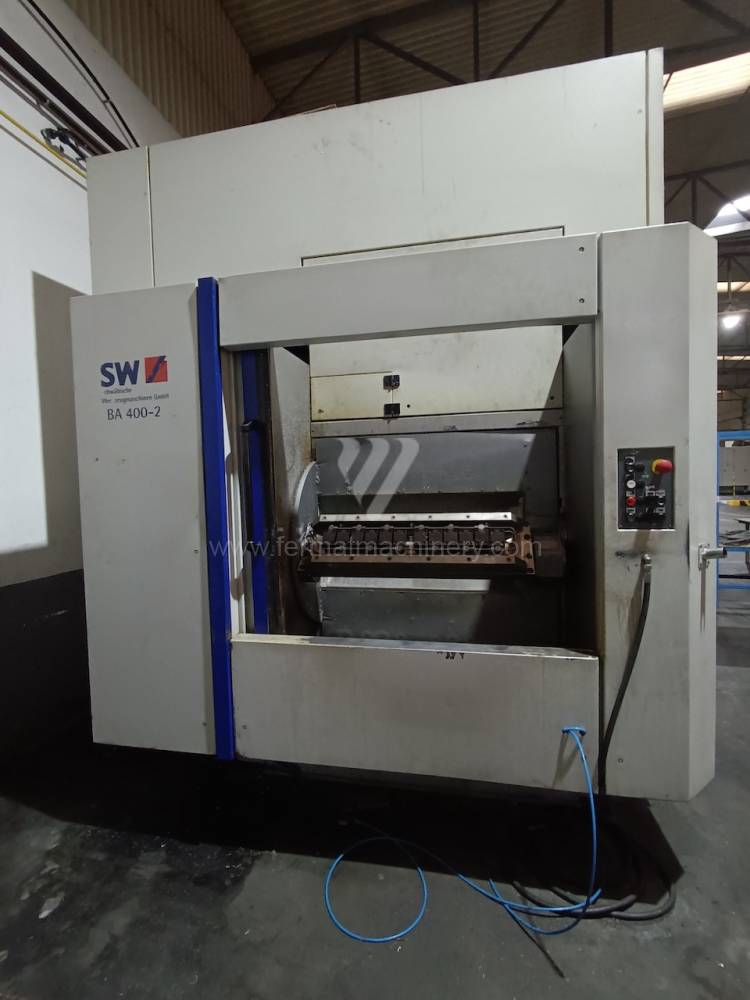 |
BA 400-2 |
251909 | SW maschinen | 2003 | Control system Siemens: Clamping area of table: mm Travel X-axis: 400 mm Travel Y-axis: 450 mm Travel Z-axis: 400 mm Spindle speed: 50 - 12500 /min. |
|
 |
VCF 850 LSR |
261569 | Doosan | 2018 | Control system Fanuc: 31i - B5 Clamping area of table: 3500x870 mm Travel X-axis: 3000 mm Travel Y-axis: 850 mm Travel Z-axis: 800 mm Spindle speed: 0 - 12000 /min. |
|
 |
DMC 635 V |
251760 | DMG | 2010 | Control system Heidenhain: TNC 530 Clamping area of table: 790 x 560 mm Travel X-axis: 635 mm Travel Y-axis: 510 mm Travel Z-axis: 460 mm Spindle speed: 20 - 8000 /min. |
For used machining centers (VMC and HMC), the primary performance indicators are the dynamic rigidity of the spindle unit and the response speed of the digital drives. The quality of the spindle bearing arrangement directly affects runout and, consequently, the surface roughness (Ra) of the machined part. Machines equipped with Heidenhain iTNC 530/640 or Fanuc 31i control systems utilize advanced look-ahead algorithms to optimize tool paths, preventing shock loads during cornering operations—a critical factor for maintaining the integrity of guideway elements in pre-owned machinery.
Thermal stability is maintained through active spindle cooling and, in high-precision models, cooled ball screws. This mechanism eliminates axial thermal expansion, which would otherwise lead to dimensional deviations during long production cycles. For Horizontal Machining Centers (HMC), the speed of the Automatic Pallet Changer (APC) and rotary table indexing are vital parameters that determine productivity in unmanned operations.
Acquiring a used machining center allows companies to achieve rapid horizontal scalability without the extreme capital expenditure associated with new technology. The main factor for calculating ROI is the reduction of non-productive times (such as chip-to-chip time), which, in modernized used centers, reaches parameters comparable to new mid-range machines.
In terms of Total Cost of Ownership (TCO), used FERMAT centers offer the advantage of lower depreciation while maintaining a high OEE (Overall Equipment Effectiveness) standard. Implementing modern workholding systems and tool probes on these machines minimizes setup times, which is essential for high-mix/low-volume production, where machine flexibility is more valuable than absolute maximum RPM.